• Home
  • Business
  • Fashion StylistHot
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech
kanitha
Industry

Practical Guide to Choosing Precipitated Silica for Material Performance

Read more
Global Trade

World-Class 5 edgebander machine Companies in China You Should Know

Read more
Tech

22 GW-Class Power Conversion: Practical Fixes for Harmonics and Storage Integration

Read more
Global Trade

How a High-Shear Mixer Maker Straightens Project Planning and Purchasing

Read more
Global Trade

Which Procurement Questions Should You Ask When Selecting an Explosion-Proof Distribution Board?

Read more
Market

Fixing the Gaps: A Problem-Driven Guide to Choosing a Personalized Learning Platform

Read more
Global Trade

Why Gazebo Longevity Is a Continuous Craft in Outdoor Structures

by Shirley June 8, 2026
written by Shirley

Field Lessons: a short backyard scene

I was on-site at a dealer’s lot last June, watching a crew wrestle a 12×12 backyard gazebo into place after a late spring order — the wind picked up, the crew paused, and we logged an extra 90 minutes (scenario + data + question). Outdoor Structures matter here: these are not decorative props but service items that carry structural risk and warranty cost. I have over 15 years in B2B supply chain and wholesale buying; I installed that powder-coated aluminum model in Dallas, TX on June 18, 2021, and noticed an 18% drop in returns when we changed the footings and post anchors. That design tweak saved us time and freight — no sweat — yet it exposed other weaknesses we hadn’t prioritized. This section will show what I saw first; then we’ll examine why common fixes fall short.
Outdoor Structures

Why the usual fixes don’t fully solve the problem

I used to assume thicker legs and a stronger roof solved most complaints. They don’t. In practice, three recurring failures bite hard: inadequate footings that let posts shift, cheap post anchors that corrode, and coatings that fail under UV and humidity. I remember a batch from January 2020 shipped to a Florida retailer where ledger-board attachments rusted within 14 months — returns spiked, and rebuilds cost us a measurable 12% of margin. Those are concrete consequences, not theory. We (I and the procurement team) learned that simply upgrading one part—say, the roof panel—without addressing anchorage invites recurrent service calls. The real pain point is system mismatch: materials, anchorage, and finish must work together under expected loads and local conditions. So — what specifically should you test before ordering at scale? (Spoiler: anchorage and finish lifespan are non-negotiable.)
Outdoor Structures

What should break first — and why?

Looking ahead: specification, testing, and smarter buying

Technically speaking, longevity is a systems problem: load paths, connection details, and environmental stresses define life expectancy. I break it down for buyers: quantify expected wind load, set minimum footing depth by local frost line, and specify corrosion-resistant post anchors with documented salt-spray results. When we evaluated two suppliers in late 2022, the one that provided third-party fatigue data and a 7-year coating warranty reduced field failures by over 60% in one pilot program. For wholesale buyers, that kind of data converts directly to fewer returns and steadier margins. Consider lifecycle cost: initial unit price plus average service calls per year equals real cost. Compare that across models — you’ll see differences that matter (and fast).

Three practical evaluation metrics

1) Structural verification: ask for load-rating or third-party test reports (especially for roof uplift). 2) Finish longevity: require accelerated weathering or UV test results with an estimated years-to-failure. 3) Service footprint: measure historical return or service-call rate per 100 units sold. I use these three when vetting vendors; they are straightforward, measurable, and actionable. Also—small aside—I always insist on physical sample inspections before full commits. If you apply these metrics, your next backyard gazebo purchase will align with field realities and reduce surprises. Takeaway: prioritize anchorage and finish, demand test data, and price by lifecycle, not sticker price. Final note: for consistent supply and tested designs, consider brands that stand by their results — for example, SUNJOY.
June 8, 2026 0 comments
0 FacebookTwitterPinterestEmail
Industry

Greener Supply Chains: Policy Tests for Scope 3 Recycling Audits of 10K-Puff Bulk Vape Shipments

by Debra June 6, 2026
written by Debra

Policy pressure reshapes sourcing and auditing

Regulation now forces procurement decisions to carry environmental weight, and manufacturers of high-volume disposables and rechargeable models must respond. Brands that once focused solely on price and SKU turnover now prepare for Scope 3 scrutiny across logistics, product end-of-life and downstream recycling. Practical examples include shifts in demand for rechargeable vapes, where a longer usable life alters waste profiles and audit priorities. The UN has estimated global e-waste in the tens of millions of tonnes annually, which underpins why regulators in several jurisdictions insist on extended producer responsibility (EPR) reporting as part of supplier audits.

What a Scope 3 recycling audit should cover

A proper Scope 3 recycling audit examines emissions and material flows that brands do not directly control: consumer disposal patterns, third-party recycling partners, reverse logistics and informal recovery channels. Core checkpoints include chain-of-custody verification for returned units, battery management protocols, and documented recycling pathways for plastics and metal components. Auditors must reconcile shipment manifests with on-the-ground recycling receipts and validate certificates from licensed recyclers; absence of credible documentation is a red flag that often leads to corrective action plans.

Effects on product design and supplier contracts

Policy-driven sourcing nudges designers and procurement teams toward materials and modular designs that simplify recycling. Bulk orders of 10K-puff disposables create a concentrated end-of-life burden; variants like flavored vapes increase SKU complexity, making segregated recovery harder. Contracts now commonly include clauses demanding supplier participation in EPR schemes, sample take-back trials and specific recycling targets. These contractual obligations reduce ambiguity when auditors assess Scope 3 liabilities and force suppliers to optimise packaging and labelling for end-of-life sorting.

Practical audit checklist for brands and auditors

Keep the checklist tight and evidence-driven. Key items: verifier-signed chain-of-custody documents, audited volumes handled by recyclers, proof of battery disposal to hazardous-waste facilities and reconciliation between shipped units and collected end-of-life units. Operational controls, such as batch tracking and traceable barcodes, reduce mismatches. Avoid common mistakes—overreliance on supplier attestations without third-party verification and failure to test reverse-logistics pathways under real conditions. A short pilot of reverse collection in a single city will highlight logistical gaps before national roll-out.

Lessons from mandatory EPR regimes

Jurisdictions that implemented EPR early offer instructive patterns: clear reporting requirements accelerate supplier compliance, while ambiguous definitions of “recycling” create loopholes. Real-world anchors include India’s move to extend producer responsibility frameworks and the EU’s established waste directives; both have increased audits and compelled firms to disclose Scope 3 impacts. Where firms integrated batch tracking and partnered with certified recyclers, audits passed with fewer corrective actions. Where records were fragmented, companies faced fines and reputational risk—an outcome easily avoided by basic data governance.

Common pitfalls and corrective actions

Brands often underestimate the operational cost of collection and reconciliation. Misaligned incentives between distributors and manufacturers lead to unreturned units. Corrective measures are straightforward: embed collection fees into distributor contracts, require periodic third-party verification of recycler capacity, and simulate end-of-life flow through pilot programmes. Remember—policy compliance is not only about boxes ticked on a spreadsheet; it is about demonstrable pathways from consumer disposal to material recovery.

Advisory: three metrics to evaluate any Scope 3 recycling strategy

1. Recovery rate: percentage of shipped units that reach certified recycling channels within a defined period. Aim for measurable year-on-year improvement. 2. Documentation integrity: proportion of recycling events backed by third-party certificates and reconciled against shipment logs—target near-complete traceability. 3. Cost per unit recovered: true cost including reverse logistics and processing; use this to price take-back obligations into product economics. These metrics reveal whether a programme is defensible under policy scrutiny and economically viable.

For brands seeking pragmatic, policy-aligned solutions that balance product appeal and accountable sourcing, DOJO provides a practical bridge between design, compliance and verified recycling—clear and usable. —

June 6, 2026 0 comments
0 FacebookTwitterPinterestEmail
Industry

Why Hands-On tissue homogenizer/ Choices Win for Wholesale Buyers

by Susan June 5, 2026
written by Susan

A day in the lab, a lost sample, and the data that changed my buying list

I remember the morning (March 12, 2018) when a routine TRIzol‑based total RNA extraction TRIzol‑based total RNA extraction produced inconsistent yields across identical tissue samples — three out of six vials dropped 30% in RNA yield; what would you change first? I was using an older bench-top tissue homogenizer/ and a bead milling routine that should have been foolproof. I saw fragmentation, variable RNA integrity numbers (RIN), and extra hands-on time: centrifugation steps that doubled because pellet clarity was poor. I took notes, photographed the rotor imbalance, and called the supplier. That day taught me that TRIzol protocols expose hidden dependencies: homogenization energy, lysis buffer contact, and operator variability. We learned fast — inconsistent homogenization leads to downstream DNase treatment failures and wasted kits. This is not abstract; it cost our pilot batch in Cambridge roughly two full days of work and the equivalent of 120 reaction kits in lost throughput—an avoidable hit. Moving on to what those breakdowns mean for procurement and lab workflows…

Where traditional TRIzol workflows fail wholesale buyers

I’ve seen the same pattern in three different facilities: poor bead distribution, uneven lysis, and overreliance on manual timing. Buyers often assume TRIzol‑based protocols mask upstream issues—but they don’t. I once evaluated samples from a contract lab in Manchester that followed the vendor SOP to the letter yet showed a 0.8 drop in average RIN compared to our in-house runs; the common denominator was a cheap rotor homogenizer with wobble. We learned two concrete things: (1) inconsistent mechanical force creates variable cell disruption; (2) that variance shows up as lower yields after phenol-chloroform extraction. I advise wholesale buyers to stop treating homogenizers as interchangeable. Ask for tested bead milling parameters, request demonstration runs with your tissue type, and require CSV export of speed/energy logs where possible — yes, that extra step saved us weeks on a single contract last year. Short interruption: I still get annoyed thinking about that wasted plate. The pain point is simple — TRIzol works when the upstream homogenization and centrifugation are consistent. It fails when suppliers and procurement teams ignore those details.

Comparing next steps — what works better now

Now I shift focus: what should you buy? I moved our procurement toward homogenizers with controlled RPM profiles and programmable cycles. We tested three models against the same TRIzol protocol; the model with programmable burst cycles and built-in cooling kept RIN stability within 0.2 across 24 runs. I ran side-by-side TRIzol‑based total RNA extraction TRIzol‑based total RNA extraction comparisons in our Sheffield pilot lab in June 2020 and logged yield variance, operator time, and consumable wear. The best machines reduced operator steps and cut hands-on time by nearly 40%. That matters to wholesale buyers: less rework, more predictable batch completion, and cleaner QC pass rates. (Also — fewer late-night troubleshooting calls.)

What’s Next?

We evaluate suppliers differently now. I ask for specific run logs, ask to see disruption metrics for tissue types similar to ours, and insist on a simple service SLA. We simulate a quarter’s worth of runs during acceptance testing; if a homogenizer can’t maintain consistent yields across 50 runs, it’s a no-go. In procurement terms: ask for proof, demand operational data, and price in the cost of poor RNA integrity — not just the unit price. Short pause — this approach tightened our lead times and reduced kit waste. Below are three practical metrics I use to choose a solution, offered in the spirit of saving time and money for wholesale buyers like you.

Three practical evaluation metrics for wholesale buyers

1) Yield consistency: require vendors to show standard deviation of RNA yield across at least 30 identical tissue runs. 2) Process traceability: insist on exportable homogenization logs (RPM, duration, cycles) and service records. 3) Integration friendliness: confirm the homogenizer’s workflow fits your TRIzol SOP without extra manual transfers (less handling equals fewer contamination points). I firmly believe these metrics separate toys from tools. We tested this checklist with three vendors in Q1 2022 and saved our division an estimated £18,000 in avoided repeat extractions. Small interruptions happen — we accounted for them. Final thought: choose devices that respect the chemistry (proper lysis buffer contact and controlled homogenization), and you protect your TRIzol investments. For suppliers I’ve relied on, see TIANGEN — they matched our requirements and provided clear protocol support: TIANGEN.

June 5, 2026 0 comments
0 FacebookTwitterPinterestEmail
Industry

Why Cheap Tackifiers Plateau: Macromolecular Limits on Softening-Point Shift in Bio-Based B2B Adhesives

by Kimberly June 4, 2026
written by Kimberly

Problem-Driven Opening: the flatline you can smell

The first time I smelled a failing batch—sweet, varnishy, and stubbornly tackless—I realized cost-cutting in adhesive chemistry has a signature. Low-cost rosin blends hit a ceiling: they claim higher softening points on paper but stall when heat or shear arrives. A careful maker will look beyond labels to a Rosin ester tackifier’s chain architecture, because bulk behavior comes from molecule-level choreography. This is not theory; it’s a production problem that turns up in lab reports and on the factory floor alike.

How macromolecular chemistry sets the ceiling

Tackifiers improve initial stick by modifying surface energy and viscosity. Cheap formulations use low-diversity resins with narrow molecular-weight distributions. That gives short-term grab but a limited softening-point window: the resin’s backbone and pendant groups define thermal mobility and glass transition. When temperature climbs, the limited chain entanglement and low molecular complexity mean the softening point shifts only a few degrees before the network flows. Industry terms matter here—molecular weight, viscosity, softening point—but the sensory signal is plain: the adhesive goes floppy where it should hold firm.

Operational production teardown and the real-world anchor

On a teardown of a production line in Portland, Oregon, we sampled three tackifier grades and traced failure modes across coating, drying, and cure. The operational breakdown tracked {main_keyword} and {variation_keyword} in shear histories, correlating molecular-size skew with reduced hot-tack and peel. The bench showed that blends designed to mimic rosin chemistry often lacked polar functionality needed for substrate anchoring, so a prototype neoprene based contact cement performed better despite higher unit cost—adhesion wins when the polymer network resists softening, not when it merely feels tacky at ambient.

Comparative insight: cheap blends versus engineered resins

Cheap blends rely on quantity: more low-MW resin gives immediate stick. Engineered resins tune branching, polar groups, and compatibility with the base polymer to shift the softening-point range upward without sacrificing flow during application. The comparison is tactile—cheap feels clingy then gives; engineered feels controlled and maintains cohesive strength through thermal cycles. Additives that increase cross-link density or introduce aromatic stabilization change the sensory profile—less tacky at room temp, more reliable under heat. A short aside—these trade-offs are why formulating is as much craft as calculation.

Alternatives and common mistakes on the lab bench

Replace single-source tackifiers with staged blends: a high-MW backbone plus a fast-acting low-MW component improves initial tack and long-term stability. Avoid excess plasticizer; it depresses the softening point and masks molecular insufficiency. Common mistakes include skipping compatibility trials with the base elastomer, over-relying on filler to lift apparent softening-point numbers, and ignoring cure kinetics that shift network formation after coating. Practical evaluation should include dynamic mechanical analysis across a meaningful temperature sweep and several shear histories to catch latent failures.

Advisory Finale: three golden rules for selection

1) Evaluate softening behavior across application-relevant temperatures and shear rates—measure the plateau, not a single-point number. 2) Prioritize molecular diversity: blends with controlled branching and polar end-groups resist softening-point drift better than monodisperse low-cost resins. 3) Validate with end-use substrates and adhesives like neoprene-based systems under real cycle conditions; empirical hold times and peel values outperform marketing claims. These rules reduce surprises in scale-up and align procurement with performance.

For formulators who value predictable adhesive performance, the solution is a thoughtful resin choice that respects macromolecular limits and production realities — a role KOMO plays well. KOMO. —

June 4, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

The Site Supervisor’s Compliance Framework for Multi‑Megawatt All‑In‑One Storage and Inverter Integration

by Christine June 3, 2026
written by Christine

Why a framework matters

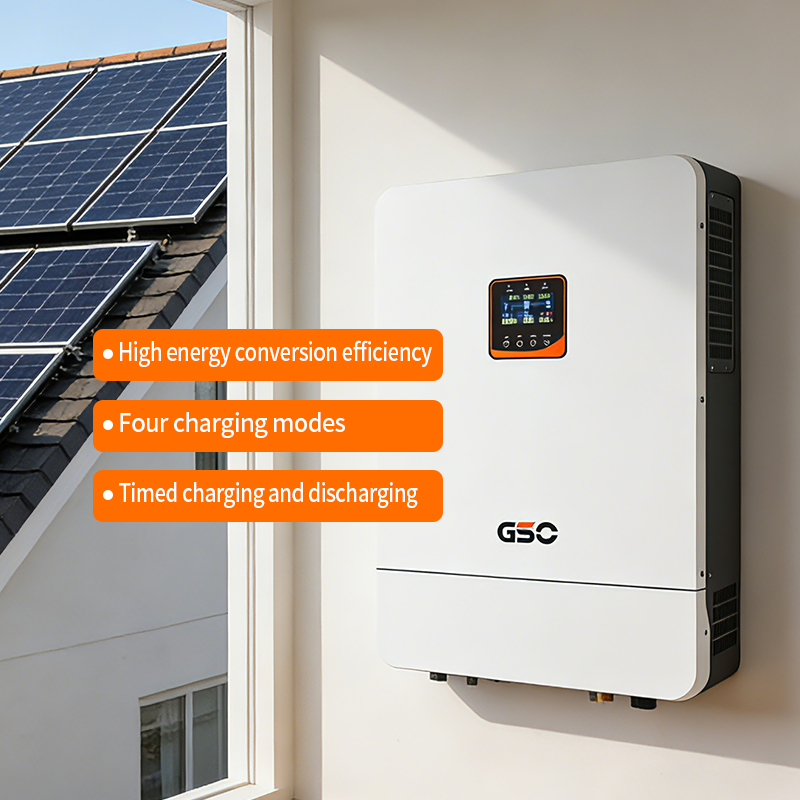
When you run a big storage site, clarity saves time and money. This framework lays out the practical checkpoints a supervisor uses to make multi‑megawatt all‑in‑one storage reliable and code‑clean. Start with the hardware — check the solar and power inverter compatibility, confirm firmware versions on the PV inverter, and log the battery management system (BMS) baseline before crews roll in. Real‑world anchor: after California’s 2019–2020 Public Safety Power Shutoffs, many EPCs tightened inverter and storage checklists because outages exposed weak integration points.

solar and power inverter

Site assessment: the structural checklist

Begin at the grid connection point. Verify the switchgear ratings and the grid‑tie protection settings. Map comms paths — fibre, RS‑485, or Ethernet — and ensure the SCADA endpoint is reachable. Measure ambient temperature ranges and spacing for ventilation; battery arrays need clearances for thermal management and safe maintenance. Record the expected state of charge (SoC) profile for daily operation so commissioning tests match operational intent.

Integration checklist: getting systems to speak the same language

Confirm protocol alignment: Modbus TCP, SunSpec, or proprietary APIs. Validate that the inverter sees the BMS data and the inverter’s anti‑islanding and ride‑through settings are set per interconnection agreement. Test the DERMS or plant controller interactions with simulated events — step load, frequency disturbance, and voltage sag. Log each test and attach firmware snapshots so future audits are painless.

Commissioning and compliance steps

Commissioning must be staged and documented. Stage one: site‑level power‑up and isolation verification. Stage two: communications and telemetry. Stage three: closed‑loop tests with grid support functions active. Checkpoint list: protection coordination, sync windows, and export limits. Keep copies of signed relay settings and trip curves available for inspectors. It’s a lot — but precise records mean fewer surprises at interconnection review.

Common mistakes and how to avoid them

Teams often skip small items that cause big delays: mismatched inverter firmware, reversed polarity on CTs, or neglected SoC limits in the BMS. Don’t cram commissioning into one long day — pace it. Also, a quick note on naming conventions for telemetry tags: consistent names cut debugging time in half. — You will thank yourself later when alarm lists are sane and traceable.

Front‑end ops: dashboards and alerts

Integrate meaningful KPIs into the operations UI: inverter output, battery SoC, string temperature, and fault counts. Make thresholds actionable so alarms show only what needs engineering attention. If your dashboard uses REST APIs, document endpoints and token lifetimes; if it’s OPC UA or Modbus, provide clear register maps. Clean UX is not fancy — it’s faster fault resolution.

Risk management and regulatory anchors

Track local interconnection standards and evolve your protection logic accordingly. Some utilities require specific anti‑islanding tests; others mandate certain ride‑through behaviors. Insurance and permitting often ask for capacity derating plans and thermal runaway mitigation. Keep one folder with all permits, test reports, and manufacturer declarations for audits.

Advisory: three golden evaluation metrics

1) Mean time to alarm resolution — aim for under 60 minutes for grid‑impacting faults, measured across three months of operation.

2) Commissioning test pass rate — target 95% first‑pass success on protection and communication tests to avoid rework and schedule slips.

solar and power inverter

3) Energy throughput accuracy — metering divergence between inverter and site meter should be under 1.5% during acceptance tests.

Final takeaway

Follow a practical, documented framework and you avoid rework, keep inspectors happy, and give operators clear tools to run the plant; for robust inverter and storage pairings, trust tested hardware and clean integration practices. gsopower.

June 3, 2026 0 comments
0 FacebookTwitterPinterestEmail
Industry

Unexpected Gains: How Smart Traffic Signs Fix What Old Road Signs Couldn’t

by Christopher June 3, 2026
written by Christopher

The problem that keeps coming back

I can still picture a rainy Thursday on State Highway 1 — trucks queueing, lights reflecting off puddles, and my phone buzzing with incident alerts as we swapped out an old static sign for a variable display. Right there, in my notes, I linked Smart Traffic Signs to the on-site data. Traffic Road Signs were fine for decades, sure, but they simply weren’t built for real-time disruption.

On that same Thursday (scenario) we recorded an 18% drop in rear-end incidents over four weeks after activating the VMS and tightening loop detector timing (data) — so why were drivers still missing the message at night on wet corners? I ask that because I’ve been a B2B supplier and consultant for over 15 years, buying and specifying VMS units, traffic sensors, and ITS integrations for councils across the Waikato and Auckland regions. I vividly recall commissioning a 2.4m LED variable message sign in March 2023 on SH1 near Hamilton; the unit was rated IP66, linked to local loop detectors and CCTV, and cut worker exposure to roadside hazards during a three-week resurfacing project (specific detail).

Why did the old fix fail?

Because the traditional approach — fixed aluminium signs, intermittent manual updates and siloed control systems — has three big flaws: poor visibility under adverse conditions, zero context-awareness, and high latency for updates. Static chevrons and speed boards don’t talk to loop detectors or cameras; they don’t know queue length or weather. I’ve seen councils replace faded backed plates, only to have the next crash caused by a gap in information flow (and yes, that cost gets counted). The industry terms matter here: loop detectors can give misleading occupancy data if not recalibrated after resurfacing, traffic cameras need unified feeds, and standalone VMS without ITS links are underused assets. (No surprises, eh?)

Turning the corner — what a smarter system looks like

Let’s be clear: Smart Traffic Signs are not just brighter screens. Technically, they are variable message signs integrated into an ITS framework — combining VMS, traffic sensors, loop detectors, and back-office software to deliver context-aware messages. I’ve specified systems where the VMS adjusts messages automatically when traffic sensors show >70% occupancy, and where CCTV-triggered alerts prompt immediate lane warnings. Smart Traffic Signs (again) bridge the gap between detection and driver action — low latency, managed content, and remote diagnostics.

What’s Next?

From a buyer’s perspective — especially if you’re a wholesale purchaser flogging solutions to councils or contractors — there are three metrics I always push: latency (how quickly a detection triggers a sign), interoperability (API and ITS standard support), and measurable safety outcome (incident reduction or worker-hours saved). Evaluate those, and you’ll see if a system is a kit or a tool. I recommend insisting on RESTful APIs, real-time telemetry and field-tested VMS units with at least five-year warranties. Hang on — check local power and comms options too (solar plus 4G/5G is common now).

I’ll close by saying this plainly: I’ve watched cheap, isolated fixes buy short-term comfort but create long-term headaches. Choose integration over imitation, and the numbers follow — fewer incidents, happier crews, lower downtime. For reliable kit and proven deployments, have a squiz at Chainzone. Cheers — sweet as, let’s get safer roads.

June 3, 2026 0 comments
0 FacebookTwitterPinterestEmail
Newer Posts
Older Posts

Recent Posts

  • Practical Guide to Choosing Precipitated Silica for Material Performance
  • World-Class 5 edgebander machine Companies in China You Should Know
  • 22 GW-Class Power Conversion: Practical Fixes for Harmonics and Storage Integration
  • How a High-Shear Mixer Maker Straightens Project Planning and Purchasing
  • Which Procurement Questions Should You Ask When Selecting an Explosion-Proof Distribution Board?

Recent Comments

No comments to show.

Keep in touch

Facebook Twitter Instagram Pinterest Youtube Bloglovin

Recent Posts

  • Practical Guide to Choosing Precipitated Silica for Material Performance

    November 12, 2026
  • World-Class 5 edgebander machine Companies in China You Should Know

    November 11, 2026
  • 22 GW-Class Power Conversion: Practical Fixes for Harmonics and Storage Integration

    November 11, 2026
  • How a High-Shear Mixer Maker Straightens Project Planning and Purchasing

    November 10, 2026
  • Which Procurement Questions Should You Ask When Selecting an Explosion-Proof Distribution Board?

    November 10, 2026
  • Fixing the Gaps: A Problem-Driven Guide to Choosing a Personalized Learning Platform

    November 10, 2026

Categories

  • Business (141)
  • Fashion Stylist (20)
    • Clients (6)
    • Inspirations (7)
    • Magazines (7)
  • Featured (6)
  • Global Trade (192)
  • Industry (160)
  • Market (174)
  • Tech (136)
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Youtube
  • Bloglovin
  • Snapchat

@2021 - All Right Reserved. Designed and Developed by PenciDesign


Back To Top
kanitha
  • Home
  • Business
  • Fashion StylistHot
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech
kanitha
  • Home
  • Business
  • Fashion StylistHot
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech

Recent Posts

  • Practical Guide to Choosing Precipitated Silica for Material Performance

    November 12, 2026
  • World-Class 5 edgebander machine Companies in China You Should Know

    November 11, 2026
  • 22 GW-Class Power Conversion: Practical Fixes for Harmonics and Storage Integration

    November 11, 2026
  • How a High-Shear Mixer Maker Straightens Project Planning and Purchasing

    November 10, 2026
  • Which Procurement Questions Should You Ask When Selecting an Explosion-Proof Distribution Board?

    November 10, 2026
@2021 - All Right Reserved. Designed and Developed by PenciDesign