• Home
  • Business
  • Fashion StylistHot
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech
kanitha
Industry

Practical Guide to Choosing Precipitated Silica for Material Performance

Read more
Global Trade

World-Class 5 edgebander machine Companies in China You Should Know

Read more
Tech

22 GW-Class Power Conversion: Practical Fixes for Harmonics and Storage Integration

Read more
Global Trade

How a High-Shear Mixer Maker Straightens Project Planning and Purchasing

Read more
Global Trade

Which Procurement Questions Should You Ask When Selecting an Explosion-Proof Distribution Board?

Read more
Market

Fixing the Gaps: A Problem-Driven Guide to Choosing a Personalized Learning Platform

Read more
Market

Can a Nema 17 Closed Loop Stepper Revolutionize Precision in Automation?

by Myla December 10, 2025
written by Myla

What’s the Buzz About Closed Loop Steppers?

I remember the first time I encountered the nema 17 closed loop stepper motor; it felt like stumbling onto a hidden gem. Here’s a fun fact: these motors can cut down on overshooting, and we’re talking a whopping 70% better than traditional open-loop steppers! So, can they really improve automation precision? If you’ve ever faced the frustration of inconsistent performance in your projects—like a misalignment in a 3D printer—you’ll know just how significant this upgrade can be.

Closed loop steppers are definitely catching heat, and they have pretty legit reasons behind it. Not only do they boast higher torque at lower speeds, but they’re also more efficient. Say goodbye to stalling issues! With real-time feedback control, I promise you’ll feel the difference in your projects.

How Do They Compare to Traditional Steppers?

Alright, let’s nerd out a bit. Traditional stepper motors are great for basic positioning tasks, but they come with serious limitations—they’re prone to losing steps and can’t really adapt to varying loads. This is where the competition heats up! The closed loop design addresses those pesky missed steps by monitoring position, reducing heat, and even keeping energy use in check. In fact, a quick trip to your local closed loop stepper motor factory might just reveal these brainy motors to you.

So, looking forward, we see manufacturers ditching those old-school stepper motors for the more reliable closed loop versions. Think about adopting advanced control algorithms; they create a more responsive and precise system. If performance is your aim—this is a no-brainer! Imagine your CNC router or robotic arm not just keeping up, but outperforming expectations! It’s game-changing.

What’s Next for Closed Loop Steppers?

As we dive deeper, let’s reflect on how closed loop stepper technology isn’t just another shiny gadget; it’s genuinely transforming industries. From 3D printing to assembly lines, these motors stand to improve not just performance, but also efficiency—saving costs over time. I can’t help but feel excited about what’s on the horizon. The industry might just see these motors becoming the standard rather than an upgrade.

In my journey, I’ve learned that when evaluating tech like this, you want to consider things like torque, accuracy, and energy consumption. Quality matters more than flashiness. For everyone on the fence about whether to invest in a closed loop system—take it from someone who’s tangled in the nitty-gritty of automation: you won’t regret it.

To wrap it all up, I’ve experienced firsthand the advantages of switching to a closed loop system. They not only boost precision but also ensure your equipment works harmoniously, leading to a smoother production flow. In the ever-shifting landscape of technology, stay smart and stay ahead by keeping quality and adaptability at the forefront. Take it from me, there’s no time like the present to make that leap!

For stepping into a more efficient future, keep an eye on innovative products from brands like Leadshine—because advancement waits for no one!
December 10, 2025 0 comments
0 FacebookTwitterPinterestEmail
Business

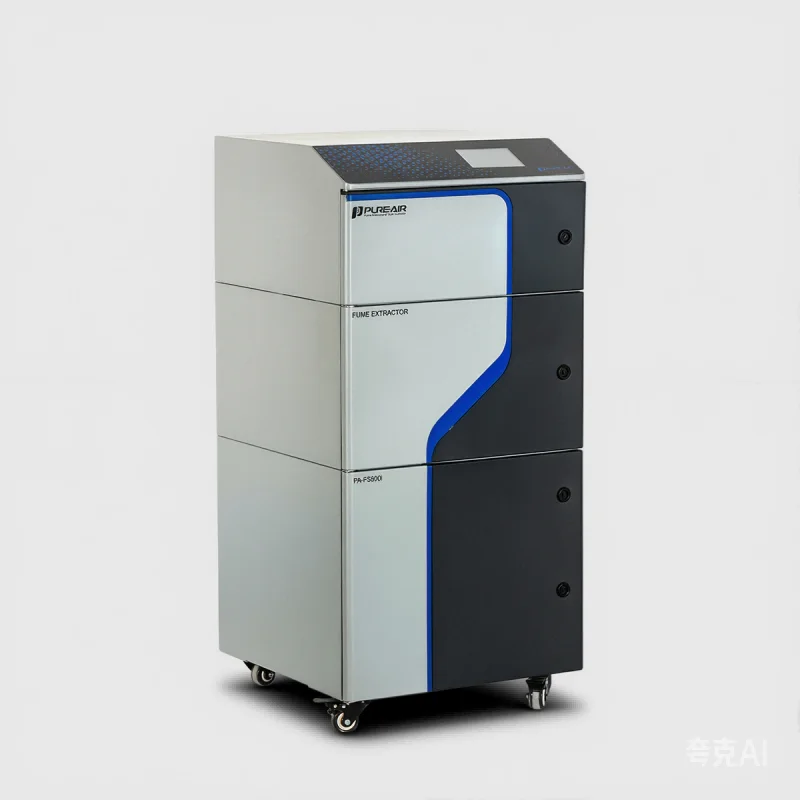
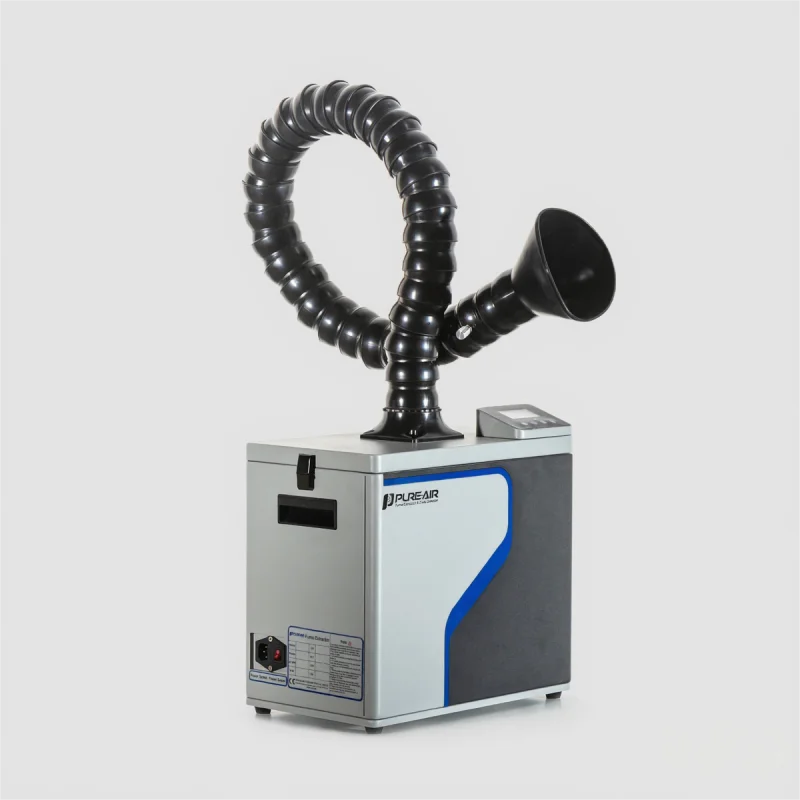
What’s the Best Method to Extract Fumes from Electronics and Industrial Soldering?

by Liam December 10, 2025
written by Liam

Introduction — why this matters now

Ever stood near a soldering line and wondered if the air you breathe is doing you harm? I have. The scene is familiar: a crowded bench, bright solder waves, and a faint chemical haze. In many factories, fume extraction for electronics and industrial applications is treated as an afterthought — yet studies show prolonged exposure raises health and compliance risks (and costs). So what practical steps actually reduce exposure on the shop floor?

fume extraction for electronics and industrial applications

I want to be blunt: the stakes are higher than managers admit. Small parts, dense assemblies, and rapid cycle times push more volatile compounds into the air. You can measure it with direct sensors, get data from local extractors, and still miss peak spikes during a shift. That leaves engineers and safety teams asking: which systems do the real work, and which just look good on paper? — a simple question, but one that needs clear answers before we buy another hood.

Below I’ll walk through the weak points I see in common systems, then move to practical, forward-looking options. Stick with me — there are fixes that don’t require a full rebuild.

Deep dive: where traditional solutions fail (technical)

wave soldering​ is central to many assembly floors. When I inspect setups around wave soldering​ lines, I often spot the same flaws. First, extraction hoods are poorly placed. They trap heat, but not the plume of fumes that rises during the solder process. Second, teams rely on undersized fans and generic HEPA filters that clog fast. Third, duct runs are long and turbulent; that kills capture efficiency. These are not minor problems — they cut capture rates in half on busy days. I say this from inspection notes and sensor logs I’ve seen firsthand.

fume extraction for electronics and industrial applications

Why does this happen? The design assumptions are old. Engineers treat fumes as a steady flow rather than bursts tied to events like conveyor speed changes or part handling. The result: negative pressure zones form unpredictably, and contaminants bypass the intake. Power converters and control panels can also add thermal loads that alter airflow. Look, it’s simpler than you think — correct placement and dynamic control matter more than raw suction. — funny how that works, right?

Why do standard extractors fail?

Because they are static systems in a dynamic process. They ignore plume behavior, transient peaks, and real operator movement. I’ve seen units that pass lab tests but fail on the line. The lesson: evaluate in situ, not in a showroom.

New principles and what to try next (semi-formal)

What’s next is about smarter capture. Rather than brute force, modern systems use real-time control and local capture close to the source. For instance, localized nozzles and segmented extraction zones respond to changes in the plume from a wave soldering​ unit. Add sensors that feed simple controllers — not full cloud suites — and you balance energy use with capture performance. Edge computing nodes can run quick decisions near the line, reducing latency and avoiding unnecessary fan run time. I’m not pushing buzzwords; I’m saying you can save money while improving safety.

Second, filter strategy needs rethinking. Combining pre-filters with targeted HEPA and activated carbon stages gives better lifetime and removal of organics. Shorter duct runs and smoother bends keep airflow stable. You will need to test with real assemblies, not coupons. I recommend staged trials: one lane with upgraded capture, another with baseline gear — compare exposure logs, maintenance hours, and energy draw. You’ll see real differences in weeks, not months.

What’s Next: implementation at scale?

Start small. Retrofit one line with source capture, add sensors, then scale if metrics improve. I prefer measurable pilots. You’ll get buy-in when downtime drops and air quality numbers improve.

Closing advice — three metrics to evaluate any fume extraction choice

Let me leave you with three practical metrics I use when advising teams. First, capture efficiency at the source: measure ppm before and after capture within the first 300 mm of the plume. Second, system responsiveness: how fast does the extraction ramp when the plume spikes? Use simple loggers to test. Third, total cost of ownership: include filter swaps, energy, and unplanned maintenance. If a vendor won’t provide real-world data or let you run a short pilot, be wary — trust is part of my rulebook, and I fail systems that hide facts.

To summarize: poor placement and static designs are the biggest pain points in wave soldering​ operations. Smarter, local capture combined with staged filtration and quick control loops gives a clear path forward. I’ve seen measurable drops in exposure and maintenance after these tweaks — results that matter to humans on the floor. For practical solutions and product options, check suppliers with field-proven systems like PURE-AIR.

December 10, 2025 0 comments
0 FacebookTwitterPinterestEmail
Industry

How PV Module + Storage Synergy Will Shape Everyday Power in 2026?

by Amelia December 9, 2025
written by Amelia

A Tuesday Brownout, a Sunny Roof, and a Better Way

Picture this: it’s a hot Tuesday, your AC is working overtime, and the grid hiccups. Lights blink, fridge mutters, pets look offended. A second later, calm. The PV module on your roof is making good power, but your home still feels fragile. Many homes now pair panels with pv and battery systems, and for good reason. Outages, even short ones, are costly in lost food, lost work, and lost patience. In many regions, peak demand days now stretch longer than they used to, and time-of-use rates bite. Yet here’s the twist: simple “backup” thinking often misses how daily loads behave. We need smarter control, not just bigger boxes.

PV module

Data tells the story. Midday solar can overshoot your use, while evening ramps hard. Average homes see spikes from compressors and induction cooktops that don’t care about your schedule. Your inverter and power converters do their best, but mismatched flows waste watts and money — funny how that works, right? So ask yourself: if solar is strong when you’re not, who is steering that energy to where and when you need it most? Let’s move from “keep the lights on” to “run the house well.” Next, we’ll unpack what actually goes sideways.

The Hidden Friction in PV + Storage You Don’t See

Where do legacy setups trip up?

Let’s be precise. Traditional AC-coupled stacks treat solar, battery, and loads as polite strangers. Energy takes extra conversions, which cut round-trip efficiency. MPPT tracking can be fine for the array yet blind to evening load shape. Inrush from HVAC hits when the battery’s state of charge is low. Result: inverter clipping, odd curtailment, and a battery that naps when it should sprint. Firmware rules often assume “backup first,” but households really need “priority by value” — keep the router, protect the fridge, shave peak price, then top up. Look, it’s simpler than you think, but only if control logic matches your actual day.

Legacy monitoring also hides costs. You see kilowatt-hours; you don’t see cycling quality or calendar aging. Without a smarter BMS that coordinates with the inverter, DC coupling strategy, and tariff windows, you over-cycle for small wins and pay later in capacity fade. Homes with EVs add another wrinkle: if the charger pulls at the wrong time, the whole plan wobbles. Bottom line: the pain points are not in the panels. They’re in orchestration — dispatch rules, conversion paths, and how your assets talk to each other when the weather and prices change by the hour.

PV module

Comparing What’s Next: Smarter Flow, Fewer Losses

What’s Next

The next wave leans into tighter integration and cleaner paths. Think hybrid inverters with DC coupling that cut needless conversions, grid-forming modes that ride through sags, and BMS logic tuned to value, not just voltage. Edge computing nodes on-site can forecast with local data, then blend weather, tariff, and occupancy signals. Dispatch becomes dynamic, not rigid. That means your array feeds the battery when price signals say “store,” and feeds the house when a compressor is about to kick. Even better, bidirectional EV chargers can serve as a big, friendly buffer — the evening peak’s worst enemy. Compared to yesterday’s boxes, the new stack wastes less and guesses less.

In practice, homes move from “backup plus hope” to “orchestrated power.” Case in point: a neighborhood pilot that tied pv and battery systems into a virtual power plant. Midday excess flowed to batteries first, then to neighbors during short ramps. Evening peaks dropped, and comfort stayed high. The lesson is simple: when controls treat a home as a small grid, not a single socket, resilience and savings rise together — funny how that works, right? So how do you choose well without getting lost in specs?

Advisory close-out: three quick metrics to compare solutions. 1) Conversion chain losses under real use (check DC vs AC paths, plus stated round-trip efficiency at partial load). 2) Control intelligence (does the system optimize by time-of-use rate, weather forecast, and device priority, and can you set rules for critical loads?). 3) Interoperability and lifespan (BMS/inverter coordination, firmware update cadence, clear warranties on cycle life and throughput). With those in hand, you can align comfort, cost, and carbon — and keep Tuesdays boring. Powered by curiosity, not hype, with a nod to LEAD.

December 9, 2025 0 comments
0 FacebookTwitterPinterestEmail
Market

Clearing the Fog: A User-Centric Guide to OTR Testers for Packaging Teams

by Mia December 8, 2025
written by Mia

Introduction — a shop-floor moment, some numbers, and the question we all ask

I was on the line one humid afternoon when a pallet of snacks came back from inspection: the products smelled stale, though they looked fine. The shift lead and I checked records and found a subtle uptick in headspace oxygen over two weeks — small, but steady. Then I asked: are we missing a testing blind spot? In many of my visits to local plants, I’ve seen the same reaction when OTR tester results don’t match shelf complaints. (You nod, then shrug; typical scene.)

Here’s the quick data slice: a handful of packs showed a 10–20% higher oxygen level than expected, and waste climbed. I thought, if the instrument readings are off, so are our decisions. So what happens next — do we spend weeks chasing uncertainty, or do we fix the root cause? I’ll share what I’ve learned from the floor, from QA meetings, and from testing labs. Expect plain talk, a few local notes, and practical steps you can try on the next shift.

Before we dig into technical bits, I’ll map the real pain points I keep seeing — and why the right test setup matters. Next up: a closer look at common flaws and why they trip teams up.

Diagnosing the deeper layer: Why standard tests miss the mark

First, let me put a tool on the table: Oxygen Transmission Rate tester. I mention it early because many of the problems trace back to how we use these machines. In my experience, operators expect a single number to answer every question. They forget variables like carrier gas quality, temperature control, and the way a sample was cut. Those factors change oxygen permeability readings fast. We end up blaming the film, the sealer, or the supplier — when really it’s the test setup that’s shaky.

Why do results vary so much?

Look, it’s simpler than you think: small leaks, an unclean permeation cell, or inconsistent film orientation will skew permeation rate and oxygen permeability figures. I’ve seen labs run tests with a calibrated leak left plugged, or—worse—without checking the carrier gas. That leads to false positives and wasted CAPA actions. From my side, the consistent offenders are poor sample handling and rushed equilibration times. If your test protocol skips a pause or ignores ambient humidity, you’ll get scatter in your data. That scatter is costly. It forces rework, extra invoices, and lost trust with customers. So I focus my training on those tiny steps that most people breeze past.

New principles and practical checks — what to adopt next

Going forward, I recommend shifting from blame to measurement design. Start with a few new principles: control the test environment, log every sample orientation, and verify zero-leak tightness before each run. When we applied these changes at one plant, variance dropped noticeably within a week — funny how that works, right? Using a calibrated Oxygen Transmission Rate tester, we also introduced a short pre-check: a blank-cell run to confirm baseline drift. That simple habit saved hours of repeat testing and a stack of paperwork.

What’s Next — three quick metrics to choose better testing solutions

If you’re evaluating upgrades or vendors, here are three metrics I trust: repeatability (how tight are repeated runs?), equilibration control (can the unit hold and log temperature and RH?), and traceable calibration (is the leak or calibration traceable to standards?). I weigh repeatability highest because stable numbers let me make decisions without second-guessing. Equally, I want equipment that logs conditions — gives me proof. Finally, calibration traceability keeps audits clean and suppliers honest. Use these as a checklist during demos and pilot runs.

In closing, I’ve seen how small process shifts save time and reduce waste. We didn’t need a miracle tool; we needed better practice and modest tech choices. If you want a practical partner in this, check Labthink — they helped my team tighten protocols without drama. I’ll keep watching how teams adapt — and I’ll share what works next.

December 8, 2025 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

Keeping Measurements Running: Five Practical Paths to Reduce Lab Balance Interruptions

by Valeria December 8, 2025
written by Valeria

Introduction — a short scene, a number, a question

One morning our routine run stalled because the bench balance drifted by 0.02 g midway through a titration — a small shift, but enough to waste three hours. I have seen this pattern many times: lab balance instruments show subtle instability, and the result is lost time and frustrated staff. Recent internal checks suggest that unpredictable downtime can cost a mid-size lab up to 6–8% of productive hours annually (yes, the number surprised me). What can we do to cut those losses and keep results trustworthy?

We will look at practical fixes and what I’ve learned working alongside bench techs and engineers. (Short notes, clear steps — that is my promise.) I will describe where common methods fail, then point forward to better principles and simple evaluation metrics. Let us begin with the parts that usually hide behind the scenes — and that often get ignored.

Where the usual fixes fail: deeper problems with lab balances

lab balances are treated like black boxes in many workflows — cleaned, zeroed, used — and then blamed when something goes wrong. In reality, there are layered issues: calibration schedules may be too loose, environmental effects are underestimated, and user handling (tare mistakes, corner loading) quietly degrades repeatability. I want to be candid: standard checklists help, but they miss the context around daily use. Look, it’s simpler than you think — small habits add up.

Let me be specific. First, calibration is often performed at fixed intervals without considering drift trends. Second, users may rely on tare and quick resets rather than checking for offset errors after moving samples from an environmental chamber. Third, the workstation itself — vibrations, drafts, thermal gradients — can create measurement variability that a single calibration won’t fix. These are not exotic problems; they are routine. When I coach teams, I push them to log small anomalies — bench vibration spikes, sample placement errors — because these logs reveal patterns that a checklist hides. — funny how that works, right?

What usually goes wrong?

Common failure modes: poor calibration strategy, mishandled tare operations, corner loading, and ignoring ambient factors. Addressing these reveals that downtime is rarely just a mechanical fault. It is a workflow and data problem combined. We must treat the balance, the user, and the environment as a system.

New principles to reduce interruptions and raise confidence

Moving forward, I favor three technology principles that change how we design procedures for balance lab equipment: proactive monitoring, adaptive calibration, and user-centered ergonomics. With proactive monitoring, you collect short, routine checks (zero stability, ambient temperature, vibration indices) and flag trends before they force a shutdown. Adaptive calibration shifts the mindset: calibrate smartly when drift patterns indicate need, not merely on a date. Ergonomics focus on training and workstation layout so corner load and improper tare are less likely. These shifts are practical and not expensive — and they scale from small labs to regulated facilities.

Implementing these principles means combining simple sensors, clear SOPs, and occasional advanced checks (repeatability tests, linearity checks). You might add a low-cost vibration sensor or keep a short log beside each bench — small moves yield big returns. I have helped labs reduce unplanned stops by encouraging micro-checks and clearer sample handling steps — and yes, that often beats waiting for the next full maintenance call. What’s next: measure the impact and iterate.

What’s Next?

Start with one pilot bench. Track stability over two weeks. If drift reduces and user errors fall, scale up. Small pilots help teams see quick wins.

Recommendations: metrics to choose and evaluate solutions

After testing, I recommend three clear metrics to evaluate any changes — these help you choose between simple fixes and larger upgrades:

1) Mean Time Between Interruptions (MTBI): Measure how often runs stop unexpectedly. A rising MTBI shows real improvement. 2) Measurement Repeatability (RSD or standard deviation): Track short-run repeatability after sample placement. If repeatability improves, you fixed handling or environmental issues. 3) Calibration Drift Rate: Log zero-offset over time; a lower drift rate means your calibration strategy is working.

Use these metrics in monthly reviews. If you pair them with targeted interventions — better calibration scheduling, small sensors for vibration and temperature, and clearer SOPs for tare and sample placement — you will see fewer interruptions and more confident results. I speak from experience: the changes are practical, and staff appreciate clearer rules — fewer surprises, calmer shifts. — and yes, I mean that.

For further detail on reliable instruments and practical support, consider the resources from Ohaus. I find their guides useful when translating principles into everyday practice.

December 8, 2025 0 comments
0 FacebookTwitterPinterestEmail
Business

Exploring the Impact of 3D Machine Vision Cameras in Today’s Industries

by Liam December 8, 2025
written by Liam

Imagine this: a factory setting where efficiency is paramount, yet defects in products have been a persistent issue. According to industry reports, nearly 30% of manufactured goods fail to meet quality standards. The integration of a 3D machine vision camera can address this pain point—bringing precision and reliability to the production process. But just how effective are these devices in enhancing manufacturing outcomes?

Flaws in Traditional Solutions

Traditional camera systems often rely on 2D imaging, which, while beneficial, can miss critical data points—especially when identifying defects in complex shapes. This limitation leads to costly reworks and downtimes, driving companies towards seeking better solutions. For instance, without depth perception, detecting misalignments or surface inaccuracies becomes a daunting task, often resulting in higher operational costs. Are organizations prepared to continue facing these challenges when a more robust alternative exists?

Principles of New Technologies

The 3D machine vision camera employs advanced techniques such as laser triangulation and structured light to deliver depth perception in imaging. This technology captures more comprehensive data, making it possible to identify and quantify defects that traditional 2D methods might overlook. Consequently, 3D machines leverage sophisticated algorithms to analyze the captured three-dimensional data instantly. This not only elevates the quality assurance standards but also translates into faster production rates across various sectors, is there any doubt about its effectiveness?

Quantified User Benefits

Users of 3D machine vision cameras report significant enhancements in operational efficiency, with an average increase of 25% in defect detection rates. Furthermore, adopting such systems has been linked with a reduction in product recalls and a boost in customer satisfaction scores. Manufacturers who have implemented these technologies find that the return on investment is realized much sooner than anticipated. So, what metrics should you evaluate when considering these solutions?

Conclusion: Evaluating Your Next Steps

When shopping for a 3D machine vision camera, always verify these three metrics: ① Image quality and resolution, ② Compatibility with existing systems, and ③ User-friendly software interfaces. These parameters are crucial in ensuring you choose a solution that not only meets your current needs but also adapts to future demands in the fast-evolving tech landscape.

Consider this: the right choice can transform your operations dramatically. For instance, a 3D camera can provide the specificity needed for exact measurements, thereby reducing the margin for error. Industries that embrace this technology are not just keeping up; they are prospering and innovating.

Moreover, implementing a 3D sensing camera can streamline processes, allowing for automatic adjustments in real-time, which can lead to significant time and cost savings. The reliability and efficiency brought by these devices make them indispensable in high-stakes environments like manufacturing and quality control.

In conclusion, the role of 3D machine vision in enhancing quality control cannot be overstated. Brands like Transfer Technology excel by providing innovative solutions that ensure operational excellence and supply chain agility. Their offerings stand at the forefront of technology, catering to businesses aiming for precision and reliability. Investing in such advanced technology is not just a choice—it’s a strategic move for future preparedness.

December 8, 2025 0 comments
0 FacebookTwitterPinterestEmail
Newer Posts
Older Posts

Recent Posts

  • Practical Guide to Choosing Precipitated Silica for Material Performance
  • World-Class 5 edgebander machine Companies in China You Should Know
  • 22 GW-Class Power Conversion: Practical Fixes for Harmonics and Storage Integration
  • How a High-Shear Mixer Maker Straightens Project Planning and Purchasing
  • Which Procurement Questions Should You Ask When Selecting an Explosion-Proof Distribution Board?

Recent Comments

No comments to show.

Keep in touch

Facebook Twitter Instagram Pinterest Youtube Bloglovin

Recent Posts

  • Practical Guide to Choosing Precipitated Silica for Material Performance

    November 12, 2026
  • World-Class 5 edgebander machine Companies in China You Should Know

    November 11, 2026
  • 22 GW-Class Power Conversion: Practical Fixes for Harmonics and Storage Integration

    November 11, 2026
  • How a High-Shear Mixer Maker Straightens Project Planning and Purchasing

    November 10, 2026
  • Which Procurement Questions Should You Ask When Selecting an Explosion-Proof Distribution Board?

    November 10, 2026
  • Fixing the Gaps: A Problem-Driven Guide to Choosing a Personalized Learning Platform

    November 10, 2026

Categories

  • Business (141)
  • Fashion Stylist (20)
    • Clients (6)
    • Inspirations (7)
    • Magazines (7)
  • Featured (6)
  • Global Trade (192)
  • Industry (160)
  • Market (174)
  • Tech (136)
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Youtube
  • Bloglovin
  • Snapchat

@2021 - All Right Reserved. Designed and Developed by PenciDesign


Back To Top
kanitha
  • Home
  • Business
  • Fashion StylistHot
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech
kanitha
  • Home
  • Business
  • Fashion StylistHot
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech

Recent Posts

  • Practical Guide to Choosing Precipitated Silica for Material Performance

    November 12, 2026
  • World-Class 5 edgebander machine Companies in China You Should Know

    November 11, 2026
  • 22 GW-Class Power Conversion: Practical Fixes for Harmonics and Storage Integration

    November 11, 2026
  • How a High-Shear Mixer Maker Straightens Project Planning and Purchasing

    November 10, 2026
  • Which Procurement Questions Should You Ask When Selecting an Explosion-Proof Distribution Board?

    November 10, 2026
@2021 - All Right Reserved. Designed and Developed by PenciDesign