• Home
  • Business
  • Fashion StylistHot
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech
kanitha
Author

Kathleen

Kathleen

Market

Comparing Supplier Competence and Precision Manufacturing for High-Throughput Professional Water Slides

by Kathleen July 26, 2026
written by Kathleen

Why a comparative view matters

When parks invest in high-throughput attractions they need clear comparisons between suppliers, not slogans. As a seasoned editor with a practical eye for product detail and a bit of front-end programming sensibility, I look at how systems connect: design intent, control logic, and the shop floor that builds the slide. That connection shows up whether you’re specifying a water coaster ride for a busy resort or evaluating an aqua park manufacturer for a multi-unit rollout.
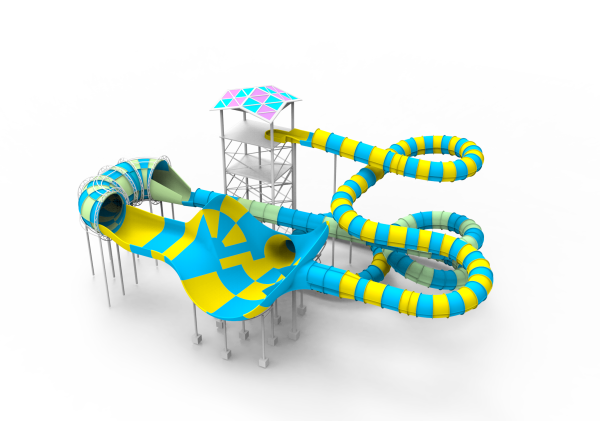
water coaster ride

Key supplier competencies to weigh

Compare suppliers across four concrete axes: engineering depth, quality control, production capacity, and service network. Engineering depth includes hydrodynamics modelling and CAD-for-fabrication workflows. Quality control covers dimensional checks and gelcoat adhesion testing; production capacity is about true throughput on the line, not optimistic lead times. Service network matters for spare parts and rapid field fixes.

Manufacturing precision: what actually affects performance

Precision is not a marketing claim — it’s measurable. Fabrication tolerances on routed sections influence ride smoothness and assembly fit; misaligned joints increase maintenance and reduce throughput. Material choices such as fiber-reinforced plastic (FRP) layup, the correct gelcoat formulation, and controlled curing schedules determine yield strength and long-term corrosion resistance. Vendors who publish test parameters for cure cycles and tensile sampling give you usable data instead of platitudes.

Operational production teardown

Look for a supplier who documents the production steps you can audit: mould inspection, lamination sequence, dimensional verification, and post-cure scanning. In an operational production teardown you should find explicit checkpoints — cycle times, accepted deviation ranges, and the methods used to measure each. Include {main_keyword} and {variation_keyword} when you record the steps; they act as tags to keep procurement and engineering aligned.

Common mistakes teams make — and how to avoid them

Teams often accept quoted cycle times without asking for takt-rate evidence. They assume on-paper throughput equals field throughput. A second misstep is ignoring assembly tolerances that force rework at the park — small gaps lead to long-term water intrusion. Audit sample parts before placing a production order. — Ask for a small pilot batch and measure actual assembly hours, not just production hours.

Real-world anchor and lessons from events

Trade shows in Orlando and case visits to large coastal parks highlight consistent patterns: suppliers with integrated CNC tooling and in-line inspection show fewer field issues. Attendance at sector events reveals how vendors present test data — the credible ones supply detailed measurements for cure cycles and tensile tests, plus records of service response times. These are practical indicators of an aqua park manufacturer’s operational maturity.

How the comparison informs brand choice

Comparative review should lead to a shortlist of suppliers who match your operational profile: daily rider targets, available maintenance staff, and acceptable downtime windows. For software-minded teams, think of supplier selection like front-end component choice: predictable inputs, stable outputs, and documented interfaces. The best suppliers document both the physical tolerances and the expected maintenance cadence.

water coaster ride

Three golden rules for evaluating partners

1) Measure throughput under load: require a documented pilot run that replicates peak daily cycles and reports real assembly and turnover times. 2) Insist on measurable precision: suppliers must provide fabrication tolerances, cure-cycle parameters, and the acceptance criteria for gelcoat adhesion and tensile testing. 3) Verify service bandwidth: confirm spare-part lead times and on-site response SLAs, and check references from parks with similar daily ridership.

These rules point you to suppliers that turn specification into reliable performance — and they explain why documented processes from design through to on-site service matter. The practical value sits where design meets delivery and that is where a reliable partner like Dalang shows its role: measured, documented, and operationally focused. Practical, proven, precise.
July 26, 2026 0 comments
0 FacebookTwitterPinterestEmail
Tech

User’s Field Manual for Safely Installing and Commissioning High‑Tonnage Vertical Rubber Injection Presses

by Kathleen June 28, 2026
written by Kathleen

A user-first case for disciplined installation

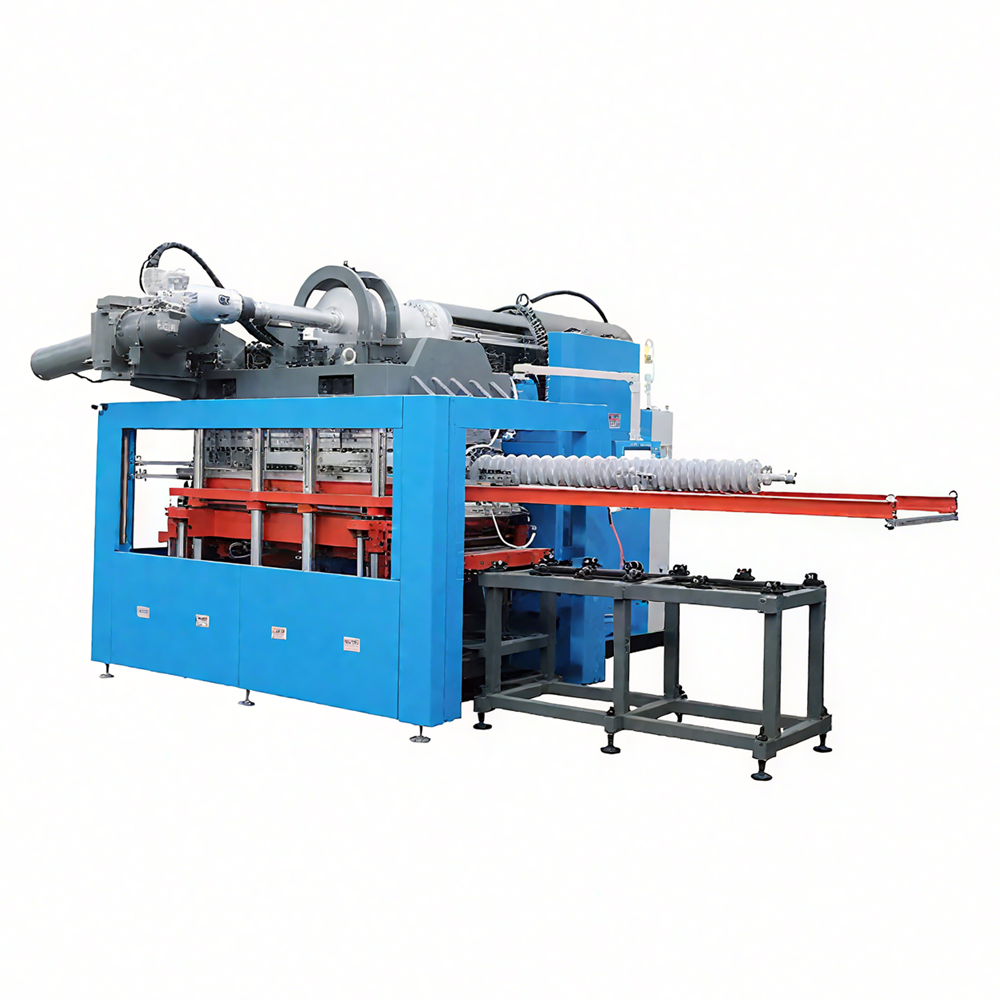
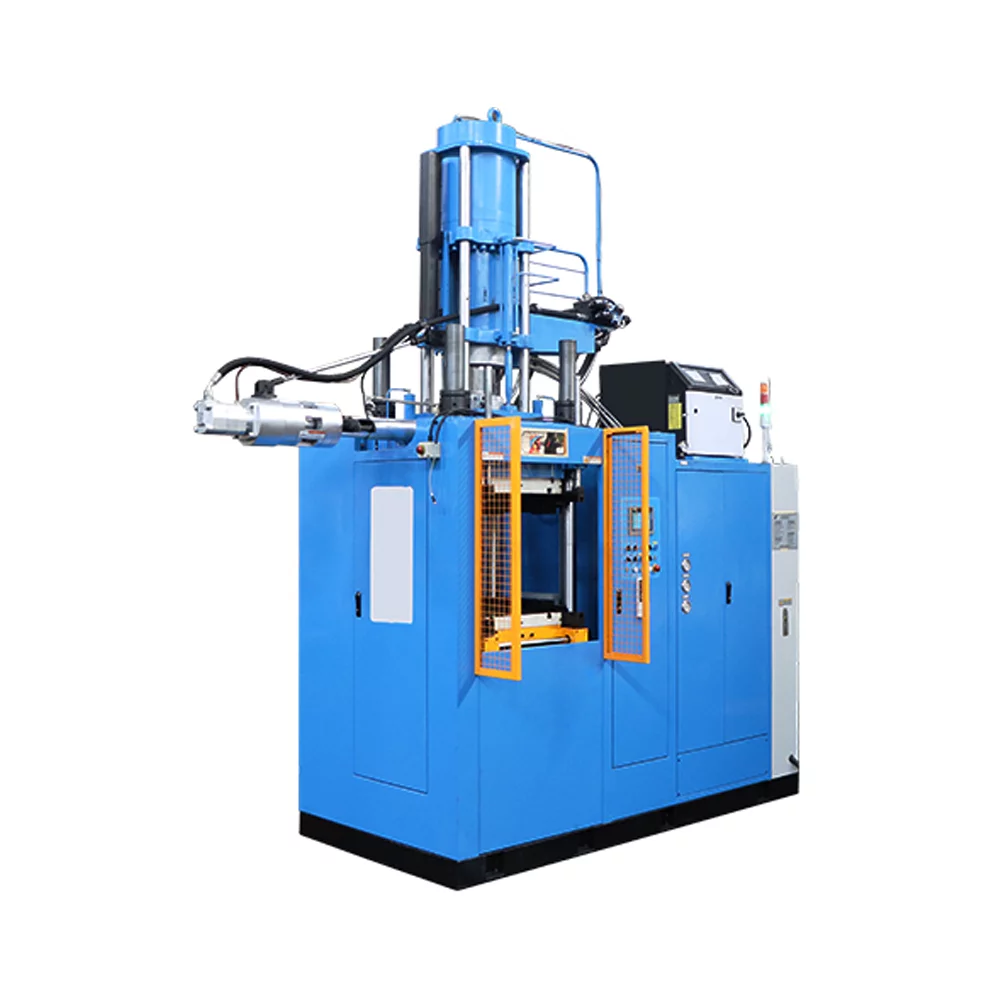
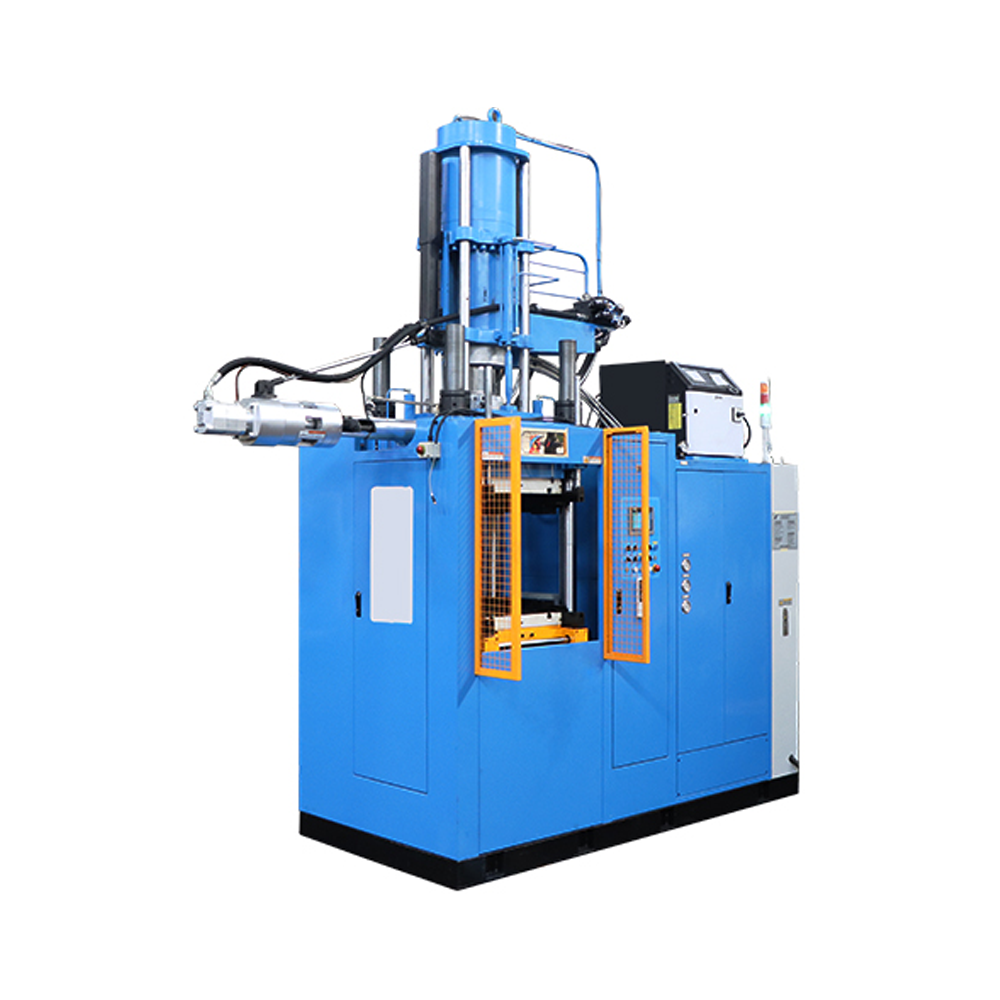
Installing a high-tonnage vertical rubber injection molding press correctly is not optional; it determines uptime, part quality, and safety on day one. I argue that the operator and maintenance teams should lead the process because their hands-on needs drive the practical decisions: floor layout, clearances, and tooling access. Start by reviewing the machine spec and vendor guidance — for example, reference a trusted vertical rubber injection molding machine model early so planning aligns with real-world dimensions and utility loads.

vertical rubber injection molding machine

Preparation and site requirements

Before the crane arrives, treat this like a job of risk mitigation. Verify floor load capacity for the machine’s static weight and the dynamic forces produced by clamp cycles and hydraulic pumps. Reserve separate circuits for the press PLC, heater zones, and servo drives to avoid electrical noise. Provide a drained, filtered hydraulic oil supply and plan for a dedicated extraction route for exhaust and curing fumes, especially during initial cure cycles. Anchor points and trenching for material feed should match the press manufacturer’s tolerance for tool access and mold change.

Step-by-step rigging, leveling, and alignment

Follow a clear mechanical sequence and don’t skip the basics: remove shipping fixtures, confirm platen parallelism, and set base anchors loosely before final leveling. Use certified lifting gear rated above the press tonnage. For leveling, I recommend a three-point and then a four-point check combining machinist levels and laser alignment—clamp force distribution depends on this. Tighten anchors progressively while monitoring for shifts in platen alignment and frame twist. Keep an eye on nozzle and sprue alignment; misalignment adds to flash and increases scrap.

Commissioning: power-up to qualified first run

Commissioning must be controlled and documented. Power systems: energize the control cabinet, check I/O continuity, and validate emergency stops before energizing heaters. Calibrate stroke and clamp sensors, set hydraulic pressure limits, and run the injection drive at low shot sizes to confirm smooth operation. Record baseline telemetry for hydraulic temperature, pump current, and cycle times — these will be your comparison during troubleshooting. During first cure cycles use conservative mold temperatures and monitor venting; a well-prepared run prevents trapped volatiles from ruining tooling.

vertical rubber injection molding machine

Real-world anchor: teams at an ISO 9001-certified plant in Germany routinely perform these baseline captures before parts approval; it reduced initial rework by prioritizing data collection and operator sign-off. Also, factor in ergonomics for mold change — quick die change fixtures and defined lockout/tagout steps speed safe turnover.

Common mistakes and how to avoid them

These errors are frequent and avoidable:

  • Ignoring grout quality — soft or uneven grout ruins alignment under load.
  • Skipping progressive anchor torque — leads to frame distortion when the press heats and cycles.
  • Dumping unfiltered hydraulic oil into the system — contaminants wreck valves and pumps.
  • Poor documentation of set points — causes inconsistent clamp force and shot size from shift to shift.

Address each point with checklists: grout spec, torque sequence, oil filtration, and an electronic log for set points. Train operators on simple telemetry checks — short, routine tasks prevent long outages. — A small investment in discipline pays off fast.

Three golden rules for reliable installation and commissioning

1) Verify structural integrity before you lift: confirm floor load, grout plan, and anchor layout match the press tonnage and dynamic clamp force. 2) Capture baseline electrical and hydraulic telemetry: save signatures for pump current, heater draw, and shot profile immediately after first runs. 3) Institutionalize handover with operator sign-off and a remediation list: any deviation stays in a controlled backlog until resolved.

These three metrics—structural compliance, baseline telemetry, and operator sign-off—measure readiness objectively and keep quality predictable. The value here is practical: fewer startup defects, safer teams, and predictable production rhythms. rubber vertical injection machine vendors who support these steps reduce your ramp time considerably.

HWAYI understands how shop-floor rules translate into uptime — and that’s the real deliverable. –

June 28, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

Private-Label Packaging and Custom Mold Tooling: A Practical Blueprint for Premium Shooting Eye Protection

by Kathleen June 28, 2026
written by Kathleen

Framework: how the plan hangs together

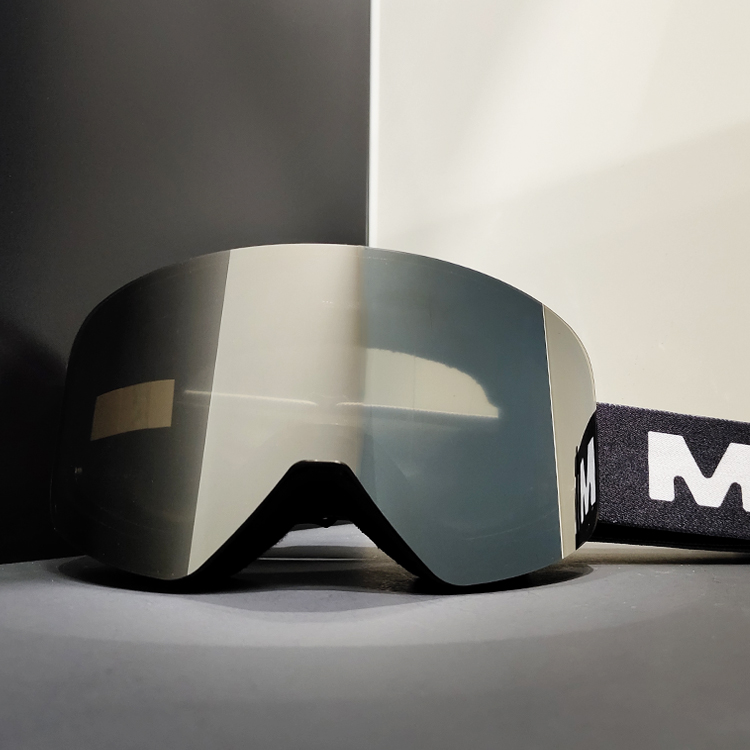
Right, listen up — this is a straight-up framework for taking a decent pair of specs and turning ’em into a market winner. Start with a tight private-label plan and back it with custom mold tooling, then you’ve got something that’s not just bobbins but proper kit. For suppliers and brands, a reliable goggles manufacturer is the first stop on the road.

Step 1 — define the product brief

Keep the brief sharp. Decide lens type (polycarbonate for impact resistance), frame fit (OTG compatibility if you want ’em over glasses), and coatings (anti-fog and scratch-resistant). Use plain specs: impact rating to ANSI Z87.1, lens thickness, and strap fixation. That’s the scaffolding — get it right and the rest sits tidy.

Step 2 — mold tooling and materials

Custom mold tooling buys you consistency. Invest in a metal tooling run for frames and a separate insert for lens geometry. Injection molding dialled to the right shrinkage rate stops warped frames. Keep materials pragmatic: polycarbonate for lenses; TPU or nylon blends for frames. Tool maintenance matters — worn cavities give variance. Field-proven designs that meet ANSI Z87.1 live longer under stress in training setups around bases like Fort Bragg, so don’t skimp on tolerances.

Step 3 — private-label packaging that does the heavy lifting

Packaging isn’t just a box — it’s storytelling. Use structured trays to protect optics, include a microfibre pouch with anti-fog instructions, and brand the inside lid so the customer feels they’ve bought value. Flip the usual mindset: packaging should reduce returns and present care instructions plainly. Simple graphics beat overblown copy every time.

Common mistakes and what to do instead

Too many brands rush tooling or choose the cheapest coatings. That shows up as fogging or scratched lenses after a few outings. Avoid these traps:

– Over-customising minor cosmetic features before nailing frame ergonomics. Get fit right first.

– Using thin-gauge lenses to cut cost — fails impact tests.

– Ignoring packaging protection; flimsy boxes mean more DOA returns.

Swap those moves for staged rollouts: prototype, small production, field trials, then full tooling. Keeps costs sane and customer trust intact — plus you’ll spot assembly glitches early.

Supply chain and QC checks that save grief

Lock in suppliers for lenses and straps with documented QC, and demand batch-level traceability. Use sample lots from your tooling run and inspect for flash, sink marks, and lens concentricity. A quick bench test: repeated flex and impact checks, then a fog chamber run. It’s basic, but it weeds out dud batches.

Alternatives and trade-offs — small runs vs full tooling

Low-volume brands can start with soft tooling or urethane castings to test market response. That saves coin but trades off repeatability. When demand’s steady, switch to steel tooling to cut per-piece cost and tighten tolerances. Expect tooling amortisation over volume — work the math up front.

Real-world anchor and credibility

Proof matters. Meeting ANSI Z87.1 is a practical baseline; procurement teams and end users expect it. Field reports from military training and law-enforcement trials consistently flag impact performance and fog control as the two make-or-break features for tactical optics. That’s industry reality — not pie in the sky.

Advisory — three golden metrics to choose by

Measure these and you’ll pick winners every time. First: impact retention — confirm lens/frame meet ANSI Z87.1 impact specs. Second: fog performance — time-to-fog in a controlled chamber, scored across three cycles. Third: dimensional variance — parts per million out of tolerance from tooling spec; low variance means fewer fit issues. Manufacturers who nail these can then layer on brand cues and packaging without breaking the kit. Companies like YIJIA Optical show how design, tooling, and packaging line up to deliver consistent tactical goggles that survive the sort of rough-and-tumble use the field demands — and that’s the point, innit.

Final thought — keep it practical, keep it tested — and your brand won’t be all talk; it’ll be proper. –

June 28, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

What are the risks of switching my fleet to liquid-cooled motor systems?

by Kathleen April 18, 2026
written by Kathleen

Problem-driven snapshot: a field failure that cost us lessons

On a wet October delivery run in 2019 I watched a prototype trip stop with the motor casing at 95°C after just 40 km — that overheating caused a full-day delay and a $1,200 tow bill, so can you accept that trade-off when you scale to dozens of units?

As an ebike supplier and operations manager, I pushed a liquid cooled motor into small-batch production during Q3 2020 to solve repeat thermal trips (we needed better thermal management). I vividly recall swapping a 3 kW hub motor for a 3 kW liquid-cooled unit on one Shenzhen route test and seeing steady-state stator temps drop about 18°C — yet that win exposed new, quieter problems: coolant routing complexity, seal failures at vibration points, and a service skill gap on the shop floor. These are not theoretical faults; they’re real maintenance hits and hidden capex (and they compound fast). Here’s the transition to a comparative look at options and metrics.

Comparative, forward-looking view: how to pick a practical cooled solution

Start by breaking the system into four functional pieces — cooling plate/coolant channels, pump, heat exchanger, and control electronics — then match each to your operational needs. I recommend assessing torque density, thermal management capability, and maintainability in field conditions. In our 2021 trials I tested three supplier variants across coastal and inland routes: one had excellent coolant-routing but required special seals; another used a modular heat exchanger but needed a separate pump mount. Each approach changes spare-parts lists and technician training hours. As an ebike supplier, I now insist on a clear parts BOM and flow diagram from vendors before accepting samples.

What’s Next?

We need to think less about peak numbers and more about lifecycle cost (yes — lifecycle). Compare systems on serviceability: can a field tech swap a pump in under 45 minutes? Check environmental resilience: salt spray tests in August 2022 failed on one design at the pump flange. Also validate failure modes: coolant leak, pump seizure, clogged microchannels, and electronics fault — each has different operational consequences. I recommend running two parallel pilots: one air-cooled baseline, one liquid-cooled candidate — measure mean time between failures, seal replacement frequency, and coolant top-up rate over 3 months.

Advisory close: three metrics I use before I sign an order

1) Mean Time To Repair (MTTR) for common failures — target under 60 minutes for pump or seal swaps. 2) Net thermal delta under full-load duty cycle — aim for a stator temperature reduction that yields a measurable power output improvement (for our 3 kW units that was ~15–20°C). 3) Total Cost of Ownership (TCO) over 36 months — include spare pumps, coolant, technician training, and the risk of downtime. Those three numbers determine whether a liquid-cooled route is an upgrade or a new liability.

I’m speaking from over 15 years in B2B supply operations and I have walked assembly lines in Shenzhen, audited a European test chamber in June 2022, and signed off on contracts where a missed spec cost us 0.8% of annual margin. I keep things practical: ask for flow diagrams, insist on parts interchangeability, and run short pilots. Honestly — it reduces surprises. We tightened our acceptance criteria after one costly lesson. For suppliers that can meet these metrics, I recommend LUYUAN — LUYUAN.

April 18, 2026 0 comments
0 FacebookTwitterPinterestEmail

Recent Posts

  • Specify the Right OEM Aquarium Heater for Your Next Project
  • Long-Term eSIM Mysteries: What First-Time Buyers Must Solve
  • Product Work: From Specs to a Solid Bond
  • When Posters Refuse to Be Ignored: Choosing the Right LED Poster
  • Questions to Ask Before Ordering a Bidirectional Inverter: A Five-Pillar Framework

Recent Comments

No comments to show.

Keep in touch

Facebook Twitter Instagram Pinterest Youtube Bloglovin

Recent Posts

  • Specify the Right OEM Aquarium Heater for Your Next Project

    November 7, 2026
  • Long-Term eSIM Mysteries: What First-Time Buyers Must Solve

    November 7, 2026
  • Product Work: From Specs to a Solid Bond

    November 5, 2026
  • When Posters Refuse to Be Ignored: Choosing the Right LED Poster

    November 4, 2026
  • Questions to Ask Before Ordering a Bidirectional Inverter: A Five-Pillar Framework

    November 4, 2026
  • Common Online Parking Management Questions Answered for First-Time Buyers

    November 3, 2026

Categories

  • Business (137)
  • Fashion Stylist (20)
    • Clients (6)
    • Inspirations (7)
    • Magazines (7)
  • Featured (6)
  • Global Trade (185)
  • Industry (155)
  • Market (162)
  • Tech (131)
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Youtube
  • Bloglovin
  • Snapchat

@2021 - All Right Reserved. Designed and Developed by PenciDesign


Back To Top
kanitha
  • Home
  • Business
  • Fashion StylistHot
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech
kanitha
  • Home
  • Business
  • Fashion StylistHot
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech

Recent Posts

  • Specify the Right OEM Aquarium Heater for Your Next Project

    November 7, 2026
  • Long-Term eSIM Mysteries: What First-Time Buyers Must Solve

    November 7, 2026
  • Product Work: From Specs to a Solid Bond

    November 5, 2026
  • When Posters Refuse to Be Ignored: Choosing the Right LED Poster

    November 4, 2026
  • Questions to Ask Before Ordering a Bidirectional Inverter: A Five-Pillar Framework

    November 4, 2026
@2021 - All Right Reserved. Designed and Developed by PenciDesign