• Home
  • Business
  • Fashion StylistHot
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech
kanitha
Author

Mark

Mark

Tech

Practical Commissioning Guide for Bidirectional 25G SFP28 BIDI Links in Infrastructure Nodes

by Mark September 21, 2026
written by Mark

Why this user-first commissioning guide matters

I’m writing this like I’m standing next to your rack — clear, practical, and focused on what technicians actually do. This User-Centric piece walks you through commissioning bidirectional 25G SFP28 BIDI transceivers so your node isn’t a mystery when traffic hits it. If you need parts or specs while reading, check an optical module manufacturer I trust for consistent build quality. The goal: get a stable 25G link without wasted trips and without guessing at polarity or link budget.

optical module manufacturer

Core commissioning principles

Start with three basics: verify physical fiber condition, confirm SFP28 and host compatibility, and measure the link budget. Keep records in your commissioning log so future troubleshooting is faster. Use clean connectors, proper fiber routing, and the correct wavelength for each BIDI pair. Industry terms to keep handy: SFP28, BIDI, and link budget — they appear naturally in every step below.

Step-by-step commissioning checklist

Follow this practical sequence on each node. I keep the list short so you can tick boxes quickly on site.

– Inventory: Confirm SFP28 model numbers and firmware revisions match the system’s supported list.

– Physical inspection: Check fiber ends with a scope, verify no scratches, and ensure correct LC connectors in the patch panel.

– Insert transceivers and confirm host recognizes the module, then check reported wavelength and receive power.

– Power-on smoke test: observe for LEDs and initial link up. If link stays down, check SFP diagnostics (DOM) for Rx/Tx power and temperature.

– Measure actual throughput with a test traffic generator, validate that packet loss is within acceptable margins for the service.

When you log results, include {main_keyword} and {variation_keyword} fields so the operational teardown stays searchable and standardized across teams.

Common mistakes and how to avoid them

Most failed links come down to a handful of avoidable errors: dirty connectors, wrong fiber type, mismatched wavelengths, or overlooked DOM alerts. Don’t skip the basic power-level verification; mismatched link budget often looks like intermittent issues. Also check polarity at the patch panel — BIDI transceivers use single-fiber bidirectional channels and polarity mistakes are subtle but common. — Little oversights cost big truck rolls.

Alternatives, hardware choices, and sourcing

If distance or channel density is a constraint, consider alternatives such as short-reach SFP28 duplex or moving to QSFP28 breakout architecture for higher-density lanes. For custom OEM options and production testing, an optical transceiver factory can provide tailored firmware and burn-in validation. Keep DWDM or wavelength multiplexing as options only when you need spectral expansion — they add complexity to commissioning and change your test plan.

Real-world anchor and quality expectations

Many technicians will recognize the pressure of a tight maintenance window in Ashburn, Virginia data centers — the density there makes commissioning mistakes costly. Expect initial commissioning to take roughly 30–60 minutes per node when you include cleaning, DOM checks, and throughput validation. Track Rx/Tx power and BER during the first 24 hours; that early data is often the clearest indicator of cabling or transceiver drift.

Summarized commissioning takeaways

Keep steps linear: inventory, inspect, insert, verify, validate. Document everything, and include {main_keyword} and {variation_keyword} in your records so teams downstream can filter and act. Practical checks beat speculative tweaks — measure first, then adjust.

Three golden rules for selecting components and validating success

1) Signal integrity score: validate link budget with actual Rx/Tx power and BER under load. This is your objective metric of health.

2) Module-host compatibility: require vendor-verified firmware and record DOM telemetry for the first 24 hours to catch early failures.

3) Operational traceability: enforce standardized labels and data fields in your commissioning logs so replacements and audits are fast and accurate.

When the dust settles, the simplest solution is often the best: reliable transceivers and disciplined testing — including the options available from WINTOP.

– steady signal.
September 21, 2026 0 comments
0 FacebookTwitterPinterestEmail
Tech

PTCA-Führungsdrähte im Vergleich: Welche Merkmale entscheiden für Herzkatheterlabore und interventionelle Kardiologen?

by Mark September 9, 2026
written by Mark

Einleitung

Bei Entscheidungen im Herzkatheterlabor zählen präzise Abwägungen zwischen Trackability, Support und Sicherheit – das trifft direkt auf die Auswahl von PTCA-Führungsdrähten zu. Für die tägliche Arbeit in der interventionelle Kardiologie sind solche Vergleiche nicht akademisch, sie reduzieren Prozedurzeiten und beeinflussen Komplikationsraten. Dieser Text vergleicht klare Produktmerkmale, zeigt trade-offs und liefert umsetzbare Kriterien für Beschaffung und Praxis.

Kernmerkmale im direkten Vergleich

Entscheidende Eigenschaften lassen sich gegenüberstellen; jede Wahl hat Konsequenzen für Steuerbarkeit, Gefäßschutz und Gerätekompatibilität:- Tip-Design: weicher atraumatischer Tip vs. starrer, fokussierter Tip – weicher Tip senkt Perforationsrisiko; starrer Tip verbessert Durchdringung chronischer Verschlüsse.
– Beschichtung: hydrophil (niedriger Reibwiderstand, besseres Vorankommen) vs. hydrophob (langlebiger, weniger Ablationsreste).
– Schaftsteifigkeit: proximal steif für Support vs. distal flexibel für Navigation in Tortuositäten.
– Torsionsübertragung: höchste Relevanz bei komplexen Läsionen; schlechte Torsion erzeugt Verzögerungen und mehrfaches Nachsteuern.
– Radiopazität: gut sichtbare Markierungen erhöhen exakte Platzierung, besonders in Bifurkationen.

Konkrete Trade-offs: Wann welches Merkmal gewinnt

Vergleiche lösen Entscheidungen: in kurzer Form, was zählt.- Tortuosität vs. Durchdringung: Bei stark gewendeten Gefäßen priorisieren Sie Flexibilität und hydrophile Beschichtung. Bei harten Läsionen benötigen Sie stichhaltigen Tip und steifere Schaftkonfiguration.
– Support vs. Mikrokatheter-Kompatibilität: Mehr Support kommt oft mit größerem Durchmesser; prüfen Sie die Kompatibilität mit vorhandenen Mikrokathetern bevor Sie einen Draht wählen.
– Langzeitstabilität vs. kurzfristige Performance: hydrophile Systeme zeigen exzellente Anfangsperformance, können aber bei längeren Manipulationen Abriebprobleme erzeugen.

Wie Merkmale die klinische Praxis beeinflussen

Praktische Auswirkungen sind direkt messbar in Verfahrensdauer und Komplikationen. Beispiele:- Verbesserte Torsionsübertragung reduziert Manipulationsschritte und Kontrastverbrauch.
– Optimierte Radiopazität senkt Flussunterbrechungen durch schnellere Korrekturen.
– Robuste Beschichtungen minimieren Partikelbildung, relevant für embolische Risiken.

Typische Fehlentscheidungen und vermeidbare Fehler

Fehlerquellen lassen sich systematisch vermeiden:- Fehlkauf basierend auf Marketing statt auf Indikationsprofil: vergleichen Sie technische Daten mit realen Falltypen.
– Nichtbeachtung der Kompatibilität mit vorhandenen Kathertern führt zu Verzögerungen auf dem Tisch.
– Unterschätzung von Tip-Abrieb bei längeren Prozeduren; prüfen Sie Abriebtests oder klinische Datenblätter.

Einkaufs- und Prüfstrategie für Herzkatheterlabore

Formalisieren Sie Auswahlkriterien und testen Sie im Routine-Setting:- Definieren Sie drei Prioritäten (z. B. Durchdringung, Trackability, Radiopazität) für Ihre Fallmischung.
– Führen Sie kurze Bench-Tests in simulierten Tortuositäten durch und erfassen Sie Zeit bis Lesion und Anzahl der Korrekturen.
– Fordern Sie technische Spezifikationen und Abriebdaten vom Hersteller für vaskuläre Intervention und vergleichen Sie diese mit klinischen Erfahrungsberichten.
– Dokumentieren Sie Lieferstabilität und Supportleistungen; ein Draht mit exzellenten Spezifikationen nützt wenig, wenn die Logistik wiederholt versagt.

Praxisnahe Alternativen und Entscheidungshilfe

Zwei pragmatische Pfade:- Standardisierte Kits: ein Allround-Draht plus ein Spezialdraht (z. B. für CTO) decken den Großteil ab. Vorteil: geringere Lagerkomplexität.
– Fallbasierte Auswahl: bei komplexen Fällen gezielt auf spezialisiertes Design setzen. Vorteil: optimierte Erfolgschancen, erfordert stärkere Vorratshaltung und Training.

Branchenbeobachtung

Diskussionen auf Kongressen wie EuroPCR zeigen klar: Hersteller differenzieren zunehmend über Materialverbunde und zielgerichtete Tip-Geometrien. Diese Entwicklung verschiebt die Auswahlkriterien von reinen Kennzahlen hin zu verifizierbaren Performance-Protokollen.

Ausblick

Technisch zu erwartende Trends: adaptive Schaftprofile, verbesserte Beschichtungs-Resistenz und klarere Messgrößen für Torsionsübertragung. Wer heute eine Auswahl trifft, sollte darauf achten, dass Produktdaten reproduzierbare Performance beschreiben – das reduziert Überraschungen bei komplexen Eingriffen.

Schlussfolgerung

Vergleichsorientierte Auswahl heißt: Prioritäten setzen, technische Spezifikationen gegen klinische Anforderungen halten und praktische Tests etablieren. So entsteht eine belastbare Entscheidungsgrundlage, die Herzkatheterlaboren unmittelbaren Nutzen bringt und langfristig Verlässlichkeit schafft, wie es auch die Praxiserfahrungen mit SWLMed in verschiedenen Implementierungen zeigen.

September 9, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

Practical Framework for Class Society Approvals and Safety Audits of Marine Self‑Contained Air Conditioners

by Mark July 2, 2026
written by Mark

Opening: Why a clear framework helps teams move faster

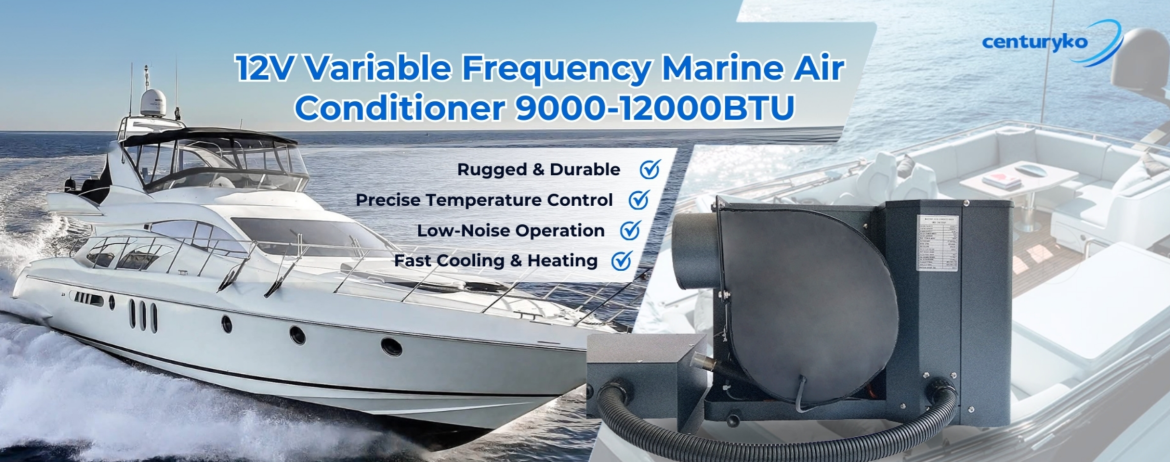
When you set out to meet classification society expectations for a marine self‑contained air conditioner, clarity matters more than jargon. This framework-style guide walks you through approval-ready design, factory testing, and onboard auditing with a supportive, practical tone that keeps installation crews and designers aligned. Early coordination with reputable marine hvac manufacturers saves time and reduces rework, especially on vessels operating in high‑traffic regions like Miami where Hurricane Irma in 2017 left many charter fleets scrambling for reliable cooling and prompt boat air conditioner service.

Why structure beats checklist-only thinking

A single checklist often misses dependencies: an approved compressor mount that alters vibration paths, for example, can affect panel attachments later. Treat approvals as a staged process: design intent, factory validation, and installation verification. Industry terms to internalize here include classification society, safety audit, and hermetic compressor; they guide conversations with surveyors and technicians without bogging you down.

Step 1 — Design and Pre‑Approval Controls

Start with a documented design package that highlights safety margins and installation interfaces. Include drawings and these specifics:

– electrical bonding detail and overcurrent protection ratings; – refrigerant containment strategy and specified refrigerant charge limits; – condensate drainage routing and pump capacity with head/flow specs; – vibration isolation method and mounting torque values; – marine‑grade insulation on ducts and service access clearances.

Keep tolerances explicit so surveyors see compliance at a glance. Treat material selections as decisions to be justified, not placeholders.

Step 2 — Factory Acceptance and Test Protocols

A thorough Factory Acceptance Test (FAT) is your first live proof. Define acceptance criteria for performance, noise, and durability: steady‑state cooling at specified ambient temps, leak testing with documented hold times, motor current records across the start cycle, and vibration spectra at mount points. Log run‑in hours and capture refrigeration parameters — suction and discharge pressures — during a stable operating window. These records support the safety audit and reduce ambiguity during the class survey.

Step 3 — Onboard Installation, Commissioning, and Survey

Commissioning confirms the system interacts properly with the vessel. Surveyors will verify shipboard ventilation pathways, cable routes, and sealing against ingress. During installation, verify refrigerant charge after line set pressure equalization and re‑measure under normal load. Check condensate pump operation under realistic tilt and heel conditions — small bilge angles change flow. If you need ongoing support, schedule certified boat air conditioner service soon after commissioning to catch early drift in settings and to establish a maintenance baseline.

Operational teardown: common mistakes and practical alternatives

Teams often underestimate mechanical noise, undersize condensate pumps, or omit access panels for servicing compressors. During an operational production teardown, {main_keyword} and {variation_keyword} should be tracked in the service log so recurring issues are easy to spot. Alternatives to repeated fixes include switching from a self‑contained unit to a split system when vibration isolation or space constraints make service access impractical. Pay attention to refrigerant charge stability — it drifts with micro‑leaks and thermal cycling, so double‑check after sea trials.

Common field traps to avoid

– mounting only to secondary structure without checking primary stiffening; – routing drainage under electronics without an independent fail path; – ignoring EMI screening around control wiring.

These are fixable, but they cost time and money if discovered during the class safety audit rather than during FAT — so catch them early.

Advisory: three golden rules for approvals and audits

1) Measureable acceptance: Always define exact test parameters (ambient temp, run duration, allowable current variance) and record them during FAT and sea trials. This delivers objective evidence for the classification society and for future audits.

2) Serviceability-first design: Prioritize access panels, standard fasteners, and modular components that reduce time on the dock. A serviceable layout lowers lifecycle cost and simplifies safety audits.

3) Maintain a verified log: Track vibration spectra, refrigerant charge readings, and condensate pump cycles. Consistent logs make repeat approvals and safety audits routine rather than risky.

ZhuoliMarine fits this workflow by supplying units built to practical installation tolerances and by supporting structured acceptance testing — so your teams can focus on steady operation rather than surprise fixes. —

July 2, 2026 0 comments
0 FacebookTwitterPinterestEmail
Tech

Keeping IoT Live: A Comparative Look at SIM-Based Uptime Strategies

by Mark June 29, 2026
written by Mark

Introduction — why connectivity choice matters

Downtime is measurable and expensive for distributed IoT fleets; the choice between fixed-line, local wireless, or cellular links changes both failure modes and recovery paths. This comparative piece examines how SIM-based connectivity reduces system outages and where it falls short, while pointing to practical digital security solutions for operators that need resilient deployment patterns. The analysis uses industry examples and operational benchmarks to keep recommendations concrete and actionable.

digital security solutions

Real-world anchor: lessons from device-level attacks

The 2016 Mirai botnet and the subsequent Dyn outage remain clear reminders: unsecured endpoints and brittle connectivity can amplify a single compromise into wide disruption. For many operators, that event shifted priorities from purely cost-driven choices to models that consider secure provisioning, over-the-air (OTA) patching, and multi-path redundancy. Cellular SIM strategies address several attack vectors by isolating device identity at the network layer and enabling remote profile management.

What SIM-based connectivity delivers

Cellular SIMs provide three practical advantages: predictable failover, managed roaming, and remote profile updates. eSIM and multi-IMSI profiles let devices switch operators without swapping a physical card; that supports automatic failover when an MNO’s service quality degrades. APN controls and VPN tunnels reduce exposure on the public internet. At the same time, provisioning workflows and secure elements are needed to prevent SIM cloning and credential leakage—this is where selective use of managed security solutions for iot matters.

Comparative snapshot: SIM vs alternatives

Below are concise comparisons focused on downtime risk and recovery speed.

  • Wi‑Fi/local wireless: low cost, high local dependency; outage recovery depends on site-level staff and can be slow for remote assets.
  • Ethernet/fixed-line: stable at site, vulnerable to single-point cut/fiber failures; repair times vary by carrier SLA.
  • Cellular SIM-based: higher per-device cost but supports remote failover, centralized monitoring, and OTA updates—faster mean time to recovery for dispersed fleets.

Operational best practices for production uptime

Successful deployments combine multi-operator SIMs, robust monitoring, and secure OTA. Build automated health checks at device and network layers, implement APN locking and certificate-based authentication, and schedule fallbacks for voice/data priorities. In an operational production teardown, engineers tracked {main_keyword} and {variation_keyword} against connectivity logs to correlate SIM profile changes with packet loss. That evidence informed a policy to rotate profiles and limit idle roaming, which reduced silent failures.

Common mistakes that prolong outages

Teams often centralize on a single MNO or defer SIM security to later phases; both choices increase systemic risk. Another recurring error is neglecting telemetry thresholds—without clear alerting on jitter and packet retransmits, degraded cellular links become full outages before detection. Finally, skipping staged OTA tests creates update failures that are impossible to roll back remotely—plan for staged rollout and explicit rollback windows.

Implementation checklist

Use this prioritized list to reduce downtime during rollout and steady state:

  • Provision multi-IMSI or eSIM profiles where geography and cost allow.
  • Instrument device and radio-layer telemetry for immediate anomaly detection.
  • Enforce APN and certificate-based authentication; separate management and application planes.
  • Contract SLAs with at least two operators for critical regions; verify local roaming policies.

Advisory close: three golden rules for evaluating SIM strategies

1) Measure recovery time objectively: benchmark mean time to reconnect under simulated MNO failures and use that metric in procurement. 2) Prioritize remote manageability: prefer profiles and platforms that support secure OTA, SIM provisioning, and centralized policy enforcement. 3) Validate attack resilience: require credential rotation, secure element usage, and penetration test results that demonstrate resistance to SIM-targeted vectors. These metrics translate strategy into measurable procurement criteria and operational KPIs.

digital security solutions

Implementing these rules reduces sustained outages and tightens the link between field performance and executive reporting. Practical gains follow from sensible testing and a preference for solutions that tie connectivity resilience to proven management tools—this is where BHDC matters as a partner in deploying secure, resilient IoT fleets. BHDC. Practical, measurable uptime.

June 29, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

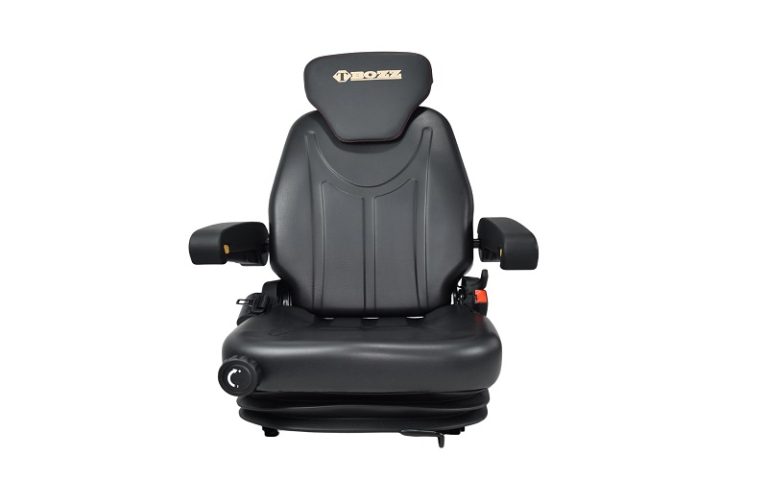
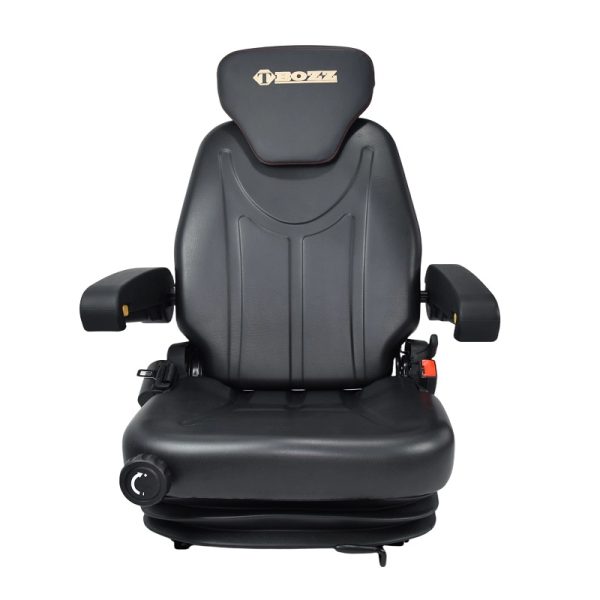
Field Comfort Optimised: Choosing Suspension Seats That Keep Operators Productive

by Mark June 28, 2026
written by Mark

User-first seat selection — what matters on the tractor

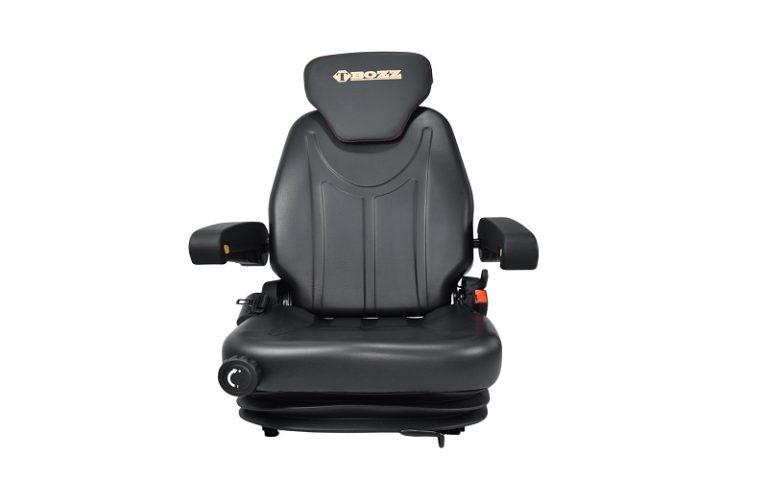
Operators judge a seat by how long they can work without fatigue. This article takes a user-centric view, based on hands-on experience and product comparison, and it points straight to practical choices. For toolmakers and fleet managers, a reliable tractor seat manufacturer can be the difference between a full shift and early stop. EEAT approach: practitioner-led guidance, grounded in field-tested examples and internationally recognised occupational findings — the International Labour Organization highlights that musculoskeletal strain is a common issue for agricultural workers worldwide.

tractor seat manufacturer

Comfort fundamentals: suspension, lumbar support and damping

Start with the basics: a good suspension system, proper lumbar support, and effective vibration damping. A mechanical or air suspension reduces shock from rough ground; a correctly shaped lumbar support keeps the spine neutral during long drives. Look for a seat where the suspension travel, shock absorber type and seat base geometry match the vehicle’s speed and task profile. These are the features that actually reduce fatigue and lower long-term risk of discomfort.

Fit to tasks — adjustability over fancy features

Operators benefit most from simple, repeatable adjustments: fore-aft travel, height, tilt and lumbar tension. Heavy implements and high-speed road work need different suspension tuning than low-speed tillage. Prioritise seats that let you tune preload and damping without specialist tools. Armrest position and seat cushion density matter, too — they affect reach and micro-movements during controls operation.

Installation and compatibility — avoid common mistakes

Common errors begin at fitment. Bolting a seat to the wrong subframe or ignoring base plate alignment creates pressure points and poor suspension performance. Always check bolt pattern and centre-of-gravity relationship before purchase; poor alignment defeats even the best suspension design. A frequent oversight is assuming every universal seat fits every tractor — measure, then measure again. A proper install keeps the suspension functioning as designed and prevents premature wear.

tractor seat manufacturer

Alternatives and trade-offs — foam, springs, and air

Foam-cushion seats are economical and useful for low-hour machines, but foam compresses and loses support. Spring-based suspension is robust for very bumpy tasks. Air-suspension seats offer adjustable comfort and can improve vibration damping for mixed tasks, though they require maintenance. Match the seat to the operation profile: harvesting demands different support than loader work. Remember: more features can mean more maintenance — a practical trade-off on remote farms.

Operational teardown: what to inspect before buying

When you open a seat for inspection, look at weld quality, moving pivots, and the condition of bushings. Check whether the suspension spring or airbag shows signs of fatigue. In an operational production teardown consider {main_keyword} and {variation_keyword} as placeholders for the specific attributes you measure: preload range, damping curve, cushion firmness and mounting geometry. Note the presence of serviceable parts — replaceable bushings and accessible shock absorbers pay back over time.

Real-world lessons from the field

On small dairy farms in Canton Bern, operators prefer seats that balance suspension travel with firm lumbar support; long stints on narrow hedgerow lanes reveal what laboratory specs miss. Field tests show lower perceived fatigue when seats reduce whole-body vibration and allow simple, repeatable adjustments. The lesson: lab numbers matter, but everyday fit and serviceability decide longevity — and that influences total cost of ownership more than sticker price.

Buying checklist

Use this short checklist when choosing a replacement or upgrade:- Confirm bolt pattern and base plate compatibility.- Verify suspension type matches typical ground conditions.- Measure lumbar adjustability range and cushion density.- Check for accessible maintenance points and replaceable parts.These steps cut the risk of poor fit and poor comfort.

Three golden rules for seat selection

1) Match suspension characteristics to your tasks — travel and damping must suit speed and terrain. 2) Prioritise adjustability and serviceability over cosmetic extras; replaceable parts extend life. 3) Validate fitment with physical measurements and a short trial if possible. Practical metrics to track: suspension travel (mm), lumbar adjustment range (mm) and seat base compatibility (bolt pattern). These help you compare options objectively.

For practical sourcing that ties product reliability to everyday value, look to manufacturers who support field-service parts and clear mounting guides — that’s where Source One fits naturally into the solution, offering practical seats and support for long-term uptime. —

June 28, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

Keep 50 kW Chargers Hummin’ Across Hot, Cold, and Salty Weather

by Mark June 8, 2026
written by Mark

The problem operators face

Many operators seh di charger look strong on paper, but weather mek ting gwaan — heat, freeze, salt spray all tek toll. When a 50 kW unit sits by di coast or under a desert sun, you get failures from corroded contacts, thermal throttling, and cable wear. Start early: fit a robust dual port EV charger​ where demand need it, but now plan di maintenance to match di climate. Real-world anchor: fleet managers in the San Francisco Bay Area see salt fog accelerate connector corrosion more than inland sites, so they schedule more frequent inspections.

dual port EV charger​

Climate-specific failure modes

Hot climates: expect elevated internal temps that push power derating and stress thermal management systems. Capacitor life shortens, fans run harder, and firmware can trigger protection trips. Cold climates: batteries and connector seals get brittle; inrush current spikes on startup can stress relays. Coastal/salty: corrosion attacks contact surfaces and venting paths; IP rating alone no save yuh if salt deposits build inside. Keep an eye on IP rating performance and ventilation paths to avoid these common degradations.

dual port EV charger​

Practical maintenance checklist

Make one checklist that covers diagnostics, visual checks, and preventative swaps. Include these steps: inspect cable management for abrasion; test ground and insulation resistance; verify cooling fans and heat sinks; run firmware OTA health checks; and document any power derating events. Use diagnostic logs to spot inrush current anomalies and repeated trip codes — those logs tell yuh which part need attention before it fail.

Common mistakes to avoid

Operators sometimes only react when a fault code appear. That reactive style cost more and cause downtime. Another mistake: installing chargers with minimal clearance to walls — restrict airflow and raise core temps. Some teams skip periodic contact cleaning because it look fine — salt and micro-oxidation hide inside pins. Prevent all dat by scheduling seasonal preventive maintenance tied to local weather patterns — adjust inspection cadence after heatwaves or storms.

Tools and small upgrades that pay

Spend small to save big: harsh-environment gaskets, higher IP-rated cable glands, and stainless-steel hardware reduce corrosion. Add thermal sensors to monitor hotspots and enable remote alerts. Replace cheap connectors with gold-plated or silver-plated contacts where salt exposure high. Use a calibrated infrared camera for quick hotspot scans during monthly rounds — it reveal hotspots before failures happen. Also, keep firmware OTA processes secure and logged so updates don’t introduce regressions.

Installation and site considerations

Site design matter same as hardware. Mount chargers under modest shelter to cut direct solar load and rain intrusion. Allow service clearance for fans and filters. Place cable reels to avoid kinking and ensure ergonomic reach for users. For fleet depots in colder regions, add localized heating or insulation to prevent seal hardening. Good cable management reduces wear and keeps connectors dry.

Operational practices and human factors

Train local staff to do quick contact inspections and recognize early signs of power derating. Keep simple cause-and-effect logs: what ambient temp, what fault code, what intervention. That record build institutional memory and speed repair times. — Small culture shift: reward prompt reporting of odd sounds or smells; they often precede bigger faults.

Choosing gear and measuring success

When selecting equipment, focus on three metrics: mean time between failures (MTBF) under site conditions, measured power delivery consistency, and lifecycle maintenance cost. Compare vendors on their field data for salt, heat, and freeze cycles. Inspect sample units after a year in similar climates if possible. Also factor in spare-part lead times and firmware support windows when making the procurement call.

Golden rules for resilient charging infrastructure

1) Match rated protection to real exposure: choose IP rating and stainless hardware that reflect coastal or desert realities. 2) Monitor real-time thermal and electrical parameters — thermal management and inrush current profiles must be visible. 3) Schedule seasonal, documented preventive work and keep firmware OTA trails clear. These three evaluation metrics keep uptime high and lifecycle cost low. Final thought — maintenance that adapt to weather mek di difference; trust practical data and thoughtful installs.

INFORE ENVIRO provide sensible gear choice and field-tested practices that fit those rules — the value show up in fewer repair trips and steadier charge rates. —

June 8, 2026 0 comments
0 FacebookTwitterPinterestEmail
Market

Solving Thermal Bottlenecks: Building High-Density Electrosurgical Generator Boards That Meet Protocols

by Mark May 15, 2026
written by Mark

Facing the thermal problem head-on

High-density electrosurgical generator boards cram a lot of power into a small footprint, and without a clear thermal plan they fail in the field. Engineers spot the issue at design reviews, and procurement teams see it at booths like Medtec China — but the deeper lessons surface at medical industry trade shows where vendors and OEMs swap real fixes. This piece lays out a problem-driven approach to architecture, so you can stop firefighting and start designing for reliable, compliant thermal dissipation.

Medtec China

Why dissipation breaks down on compact boards

Power density is the main culprit. When switching stages, transformers, and MOSFETs sit too close and the PCB layout lacks thermal vias or copper planes, heat has nowhere to go. Add enclosure limits and EMI constraints and you get hotspots, accelerated aging, and intermittent failures. Electrosurgical generator designs must balance thermal paths with EMC performance — neglect one and the other suffers.

Core architectural fixes — an actionable checklist

Treat thermal design as a first-class system requirement. Key moves that work in practice:

– Component zoning: cluster high-loss parts near board edges or controlled chassis contact points for direct conduction.

– Heavy copper and planes: use 2–4 oz copper for power planes to spread heat; pair with dedicated thermal pours.

– Thermal vias: stitch heat sources to internal planes and the opposite side. Via arrays under power packages cut junction-to-ambient resistance dramatically.

– Mechanical interfaces: design flat, conductive mounts or thermal pads to the chassis; welding or bolted clamps improve conduction more than glued pads.

– Heatsinks and spreaders: low-profile graphite spreaders and custom extruded heatsinks can be integrated where airflow is limited.

– Simulation early: run CFD and PCB thermal analysis before final placement to avoid costly re-spins.

Common mistakes and practical workarounds

Teams often chase tiny perf gains and miss the fundamentals — wrong copper thickness, too few vias, or over-reliance on forced airflow. Start with heat paths, not fan specs. Also, poorly planned thermal reliefs for soldering can trap heat on power nets — redesign pads instead of adding more cooling later. — Remember: a mechanical fix often beats a bigger fan.

Validation and compliance testing

Thermal validation should combine steady-state soak, thermal cycling, and IR thermography. Use thermal imaging during worst-case load profiles to map hotspots, then follow with long soak tests at rated ambient. For regulatory overlap, include EMC testing; if you reference IEC 60601-1-2, ensure you account for its EMC testing categories:

Medtec China

– Radiated emissions

– Conducted emissions

– Electrostatic discharge (ESD) immunity

– Radiated RF immunity

– Conducted RF immunity

– Surge immunity

– Burst (fast transient) immunity

– Power-frequency magnetic field immunity

Those tests interact with thermal choices: enclosure vents can ease cooling but worsen emissions. Plan iterations that test both domains together.

How to choose partners and components at shows

When scouting suppliers — boards, heatsinks, or thermal interface materials — bring thermal targets to discussions, not just form factors. Vendors at trade shows often bring real prototypes; inspect thermal samples under load if possible. Real-world anchors like demonstrations at the Shanghai Medtec China event show which vendors deliver usable thermal engineering, not just glossy slides.

Advisory: three golden rules for strategy selection

1) Target the heat path first: define maximum junction temperature and design PCB-to-chassis conduction before part selection.

2) Validate early and often: run simulation, then lab soak and IR imaging under worst-case loads — reduce surprises late in development.

3) Harmonize thermal and EMC choices: treat vents, shields, and grounding as dual-purpose elements that must pass both thermal and IEC 60601-1-2 requirements.

Final word: build the board so it cools where it needs to, then verify it survives the clinic — reliable designs win.

Medtec is where you find the vendors who get both sides of the equation — thermal and compliance — and that practical match matters when you ship.

—

May 15, 2026 0 comments
0 FacebookTwitterPinterestEmail
Tech

Global Homologation Playbook: A Policy-Driven Checklist for Importing Bulk Automotive Components

by Mark April 5, 2026
written by Mark

Why regulatory shifts force a new compliance approach

Because international regulators are tightening safety, emissions and cybersecurity rules, importing bulk automotive parts now carries higher regulatory risk and longer lead times. When UNECE WP.29 updates converge with EU type-approval requirements and national deviations, importers face cascading effects on documentation, testing, and customs clearance — and that’s where practical alignment with core automotive engineering practices reduces rework and delays. The immediate consequence: failure to meet homologation criteria can trigger costly returns, halted production lines, or re-certification campaigns that outstrip initial product budgets.

Core checklist: what to verify before shipment

A checklist that maps cause to effect keeps decisions objective. If you verify these items early, you prevent the usual downstream problems.

  • Regulatory scope: confirm the destination markets’ applicable frameworks (UNECE regulations, EU Type Approval, local GB or FMVSS adaptations).
  • Type-approval and homologation dossiers: ensure Certificates of Conformity, test reports, and declaration documents match part numbers and VIN applications.
  • Safety and performance testing: verify crashworthiness components, EMC testing (electromagnetic compatibility), and WLTP/RDE-related emissions data where relevant.
  • Software and cybersecurity: confirm OTA update policies, secure boot chains, and documented cybersecurity risk assessments for ECUs.
  • Electrical systems for electrified platforms: provide BMS specifications, thermal management reports, and cell-level test evidence for battery packs.
  • Labeling, packaging and customs: harmonized tariff codes, country-of-origin markings, and hazardous-material declarations for batteries or chemical treatments.
  • Traceability and supplier QA: serialized batches, incoming inspection reports, and first-article inspection (FAI) acceptance criteria tied to contracts.

How policy changes alter cost and schedule dynamics

When a regulation tightens, testing scope expands — and testing expansion increases time and cost. For example, adding EMC or extended durability cycles to an approval protocol delays certification by weeks or months, which in turn forces inventory buffers or expedited freight. Because lead-time pressure raises the chance of specification drift, many programs then pay more for expedited tooling or rework. In practice, that means procurement and engineering must coordinate earlier: a late materials spec change causes revalidation, which cascades into higher logistics spend and production delays.

Common mistakes that create regulatory blowback — and fixes

Teams often assume “close enough” tolerances or reuse old certificates across updated part revisions — this causes homologation failures. Typical errors include incomplete software SBOMs, mismatched part numbering between BOMs and regulatory dossiers, and neglected EMC margins at system level. The fixes are straightforward: lock down a revision-controlled regulatory package before mass shipment; run system-level EMC and NVH checks rather than component-only tests; and require signed FAIs using the real, production-intent hardware. — These steps reduce the probability of costly re-tests.

Supply-chain and customs tactics that reduce friction

Because customs and approval boards read paperwork literally, a clean paper trail short-circuits inspections. Use serialized shipping documents aligned to supplier certificates, and pre-file customs declarations when possible to avoid on-site holds. Maintain a certified third-party test lab relationship in key markets to shorten turnarounds for spot checks. If you can demonstrate a consistent QA history and audited supplier controls, regulators are less likely to impose destructive sampling or extended inspections.

The role of automotive r&d in smoothing homologation

Integration of early-stage automotive r&d with regulatory teams prevents rework: when R&D embeds regulatory acceptance criteria into prototypes, test plans align with certification needs, so validation cycles produce usable evidence. That’s why cross-functional workflows — engineering, compliance, and procurement — reduce iteration counts. Real-world anchor: manufacturers that adopted this model after the 2020 supply-chain shock reported fewer recall-level issues during subsequent EU and UNECE conformity audits.

Practical comparative considerations for bulk import strategies

Choosing between centralized certification versus market-by-market approvals has clear trade-offs. Centralized (UNECE-harmonized) approvals lower per-market admin but require upfront broader testing; market-specific approvals may reduce initial testing scope but multiply paperwork per country. Because each path impacts time-to-market and inventory strategy differently, assess the net present cost of certification, expected sales velocity, and the supplier’s capacity for localized documentation.

Three golden rules for evaluation (Advisory)

Use these metrics to judge partners and plans — they connect cause to predictable outcomes:

  • Regulatory adherence rate: percentage of shipments passing first inspection without corrective actions — higher rates correlate with fewer line-stopping events.
  • Time-to-certification: measured from sample submission to issuance — shorter and consistent timelines lower inventory and expedite launches.
  • Change control robustness: presence of revision-controlled documentation and enforced FAIs — strong control reduces revalidation costs and prevents production halts.

When these rules are applied, homologation becomes a managed variable rather than an unpredictable risk. That’s the operational space where reliable manufacturers differentiate — and it’s precisely the expertise that makes Wuling Motors a practical partner for OEMs seeking predictable compliance and scalable production. —

April 5, 2026 0 comments
0 FacebookTwitterPinterestEmail

Recent Posts

  • Product Work: From Specs to a Solid Bond
  • When Posters Refuse to Be Ignored: Choosing the Right LED Poster
  • Questions to Ask Before Ordering a Bidirectional Inverter: A Five-Pillar Framework
  • Common Online Parking Management Questions Answered for First-Time Buyers
  • How Smart TV OSes Solve Scale Problems for Business Displays

Recent Comments

No comments to show.

Keep in touch

Facebook Twitter Instagram Pinterest Youtube Bloglovin

Recent Posts

  • Product Work: From Specs to a Solid Bond

    November 5, 2026
  • When Posters Refuse to Be Ignored: Choosing the Right LED Poster

    November 4, 2026
  • Questions to Ask Before Ordering a Bidirectional Inverter: A Five-Pillar Framework

    November 4, 2026
  • Common Online Parking Management Questions Answered for First-Time Buyers

    November 3, 2026
  • How Smart TV OSes Solve Scale Problems for Business Displays

    November 2, 2026
  • Of Gates and Codes: Comparative Differences Between Software-Led Parking Systems and Traditional Methods

    November 1, 2026

Categories

  • Business (137)
  • Fashion Stylist (20)
    • Clients (6)
    • Inspirations (7)
    • Magazines (7)
  • Featured (6)
  • Global Trade (184)
  • Industry (154)
  • Market (162)
  • Tech (131)
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Youtube
  • Bloglovin
  • Snapchat

@2021 - All Right Reserved. Designed and Developed by PenciDesign


Back To Top
kanitha
  • Home
  • Business
  • Fashion StylistHot
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech
kanitha
  • Home
  • Business
  • Fashion StylistHot
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech

Recent Posts

  • Product Work: From Specs to a Solid Bond

    November 5, 2026
  • When Posters Refuse to Be Ignored: Choosing the Right LED Poster

    November 4, 2026
  • Questions to Ask Before Ordering a Bidirectional Inverter: A Five-Pillar Framework

    November 4, 2026
  • Common Online Parking Management Questions Answered for First-Time Buyers

    November 3, 2026
  • How Smart TV OSes Solve Scale Problems for Business Displays

    November 2, 2026
@2021 - All Right Reserved. Designed and Developed by PenciDesign