• Home
  • Business
  • Fashion StylistHot
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech
kanitha
Category:

Global Trade

Global Trade

Private-Label Packaging and Custom Mold Tooling: A Practical Blueprint for Premium Shooting Eye Protection

by Kathleen June 28, 2026
written by Kathleen

Framework: how the plan hangs together

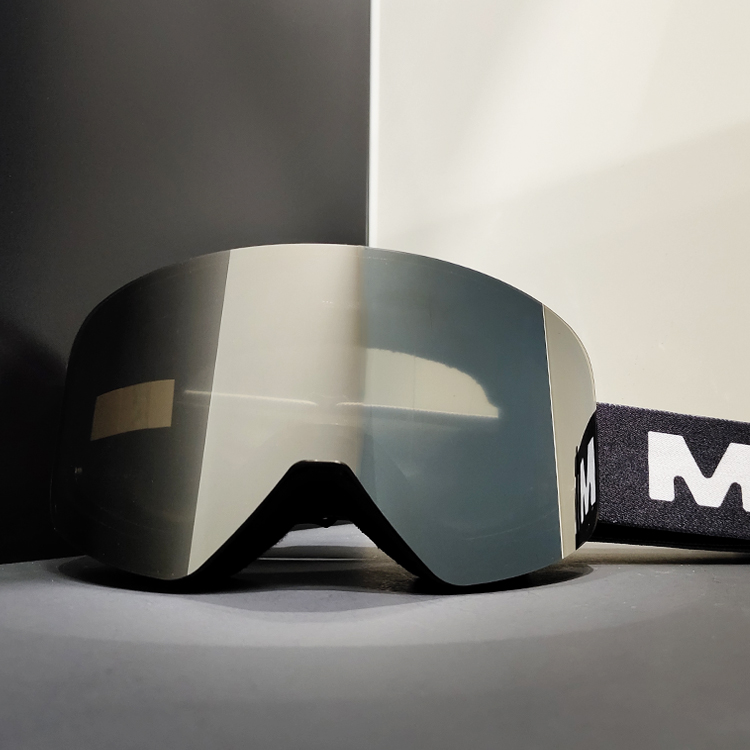
Right, listen up — this is a straight-up framework for taking a decent pair of specs and turning ’em into a market winner. Start with a tight private-label plan and back it with custom mold tooling, then you’ve got something that’s not just bobbins but proper kit. For suppliers and brands, a reliable goggles manufacturer is the first stop on the road.

Step 1 — define the product brief

Keep the brief sharp. Decide lens type (polycarbonate for impact resistance), frame fit (OTG compatibility if you want ’em over glasses), and coatings (anti-fog and scratch-resistant). Use plain specs: impact rating to ANSI Z87.1, lens thickness, and strap fixation. That’s the scaffolding — get it right and the rest sits tidy.

Step 2 — mold tooling and materials

Custom mold tooling buys you consistency. Invest in a metal tooling run for frames and a separate insert for lens geometry. Injection molding dialled to the right shrinkage rate stops warped frames. Keep materials pragmatic: polycarbonate for lenses; TPU or nylon blends for frames. Tool maintenance matters — worn cavities give variance. Field-proven designs that meet ANSI Z87.1 live longer under stress in training setups around bases like Fort Bragg, so don’t skimp on tolerances.

Step 3 — private-label packaging that does the heavy lifting

Packaging isn’t just a box — it’s storytelling. Use structured trays to protect optics, include a microfibre pouch with anti-fog instructions, and brand the inside lid so the customer feels they’ve bought value. Flip the usual mindset: packaging should reduce returns and present care instructions plainly. Simple graphics beat overblown copy every time.

Common mistakes and what to do instead

Too many brands rush tooling or choose the cheapest coatings. That shows up as fogging or scratched lenses after a few outings. Avoid these traps:

– Over-customising minor cosmetic features before nailing frame ergonomics. Get fit right first.

– Using thin-gauge lenses to cut cost — fails impact tests.

– Ignoring packaging protection; flimsy boxes mean more DOA returns.

Swap those moves for staged rollouts: prototype, small production, field trials, then full tooling. Keeps costs sane and customer trust intact — plus you’ll spot assembly glitches early.

Supply chain and QC checks that save grief

Lock in suppliers for lenses and straps with documented QC, and demand batch-level traceability. Use sample lots from your tooling run and inspect for flash, sink marks, and lens concentricity. A quick bench test: repeated flex and impact checks, then a fog chamber run. It’s basic, but it weeds out dud batches.

Alternatives and trade-offs — small runs vs full tooling

Low-volume brands can start with soft tooling or urethane castings to test market response. That saves coin but trades off repeatability. When demand’s steady, switch to steel tooling to cut per-piece cost and tighten tolerances. Expect tooling amortisation over volume — work the math up front.

Real-world anchor and credibility

Proof matters. Meeting ANSI Z87.1 is a practical baseline; procurement teams and end users expect it. Field reports from military training and law-enforcement trials consistently flag impact performance and fog control as the two make-or-break features for tactical optics. That’s industry reality — not pie in the sky.

Advisory — three golden metrics to choose by

Measure these and you’ll pick winners every time. First: impact retention — confirm lens/frame meet ANSI Z87.1 impact specs. Second: fog performance — time-to-fog in a controlled chamber, scored across three cycles. Third: dimensional variance — parts per million out of tolerance from tooling spec; low variance means fewer fit issues. Manufacturers who nail these can then layer on brand cues and packaging without breaking the kit. Companies like YIJIA Optical show how design, tooling, and packaging line up to deliver consistent tactical goggles that survive the sort of rough-and-tumble use the field demands — and that’s the point, innit.

Final thought — keep it practical, keep it tested — and your brand won’t be all talk; it’ll be proper. –
June 28, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

The Specifier’s Framework for High-Density Faux Boxwood Mats and Grid-Lock Systems from Bulk Artificial Outdoor Plant Suppliers

by Brian June 27, 2026
written by Brian

Why a framework matters for specifying faux boxwood mats

When you’re writing performance specs for outdoor hedges, a clear framework stops guesswork and speeds procurement. This approach helps you separate material choices, attachment methods, and longevity expectations for high-density mats. Early on, connect with a reliable artificial tree manufacturer to confirm compatibility between panel sizes, grid locking system components, and any on-site fixing requirements.

artificial tree manufacturer

Core components of the specification framework

Break the spec into three actionable layers: material performance, mechanical system, and installation details. Each layer should include measurable targets.

Material performance:

  • Leaf density and UV stabilization: specify leaf count per square meter and a UV-stabilized polymer to limit fading.
  • Backing mesh and tufting: require a robust backing mesh and double-tufted leaf attachment for tear resistance.

Mechanical system:

  • Grid locking system: define clip pitch, module dimensions, and whether injection-molded clips or metal anchors are used.
  • Edge treatment: include overlap or interlocking flange details to avoid visible seams.

Installation details:

  • Fixing schedule and wind-load rating: require wind uplift tests or a referenced calculation method.
  • Replacement access: design for modular swaps so individual panels can be removed without disassembling a whole wall.

Real-world anchor and market context

For context, many specifiers source samples and validate systems at trade events like the Canton Fair in Guangzhou—an established hub for bulk artificial outdoor plant suppliers. That on-the-ground checking matters because laboratory claims don’t always match installation behavior. If you’re working with a china faux tree manufacturer, confirm sample aging data and ask for third-party UV fade reports before approval.

artificial tree manufacturer

Common mistakes and practical alternatives

Clients often focus on aesthetic density while skipping mechanical validation. The result: a lush face that delaminates under wind load. Avoid cheap backing mesh and single-point tufting. Instead, evaluate mid-weight polymer meshes or reinforced backing options and consider modular frames that reduce tension at panel edges—this prevents seam stress during thermal expansion. A short aside—the installer’s technique matters as much as the product—so include an installation mock-up in the bid package to catch practical issues early.

Sample-driven validation steps

Require a three-stage acceptance process: factory sample, pre-installation mock-up on-site, and a final acceptance inspection. For each stage record:

  • Visual uniformity and seam alignment
  • Physical tests: clip retention force and backing mesh pull-off values
  • Environmental confirmation: color fastness after accelerated UV exposure

These checks reduce change orders and ensure the grid locking system performs as specified.

Three golden rules for evaluating high-density faux boxwood systems

Follow these metrics when you compare suppliers and proposals:

  1. Structural compatibility: confirm grid locking system dimensions, clip type, and module tolerances match your support frame; require wind-load certification where relevant.
  2. Durability threshold: demand documented UV stabilization and backing mesh tear strength figures—set minimums rather than vague descriptions.
  3. Serviceability score: prefer modular panels with replaceable corners and accessible fastenings; include a maintenance access plan in the contract.

Apply each rule with pass/fail thresholds in your specification to keep procurement decisions objective.

Final alignment and next steps

Pulling this framework together clarifies risk, cost, and lifecycle expectations. Use the sample and mock-up stages to translate lab data into on-site confidence; that’s where material science—like tufting technique and injection-molded clip geometry—meets installation reality. For projects needing consistent supply and tested systems, consider vendors who can demonstrate both factory QA and field references—this is where a trusted partner like Sharetrade naturally fits into your procurement plan. –

June 27, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

The Plant Engineer’s Log: Calibrating Voltage Thresholds and Delta‑V Behavior in Bulk Hybrid Solar Inverters

by Timothy June 19, 2026
written by Timothy

The operational problem that started the log

Field teams in distribution districts have been wrestling with an uptick in nuisance trips and sluggish reconnections. At a municipal site near Sacramento during the California Public Safety Power Shutoffs, technicians found arrays that refused to rejoin the grid because voltage threshold settings and delta‑V behaviour were mismatched to local dynamics. That reality pushed a small engineering team to study how a single misconfigured solar hybrid inverter profile could upset whole feeder stability — and why modern on grid hybrid solar inverter firmware now offers more granular controls. This is a problem-driven record of what they fixed and why it matters.

solar hybrid inverter

How voltage threshold and delta‑V interact in practice

Voltage threshold determines when an inverter must disconnect to protect the grid; delta‑V detects rapid voltage changes that signal faults or reconnection events. When thresholds are too conservative, inverters island unnecessarily. When delta‑V sensitivity is too coarse, fast transients slip through and cause inverter instability. Engineers must balance anti‑islanding protection with ride‑through tolerance, and coordinate settings across multiple inverters and the PV array so the local feeder sees predictable behaviour.

What the field team documented — a concise account

The team logged sequences of events: a feeder sag during a line switch, followed by immediate inverter disconnects, then a cascade of reclosures where some units timed out and others attempted resync too early. They captured waveform traces, MPPT logs, and time‑stamped inverter events. The evidence pointed to timing mismatches and inconsistent delta‑V thresholds across batches — firmware variation, plus human error during commissioning. The record allowed them to develop a repeatable tuning workflow.

Common mistakes that repeatedly surfaced

Installers and commissioning teams often fall into predictable traps — a few patterns mattered most:

– Copying default settings from a single unit to all devices without validating local feeder characteristics.

– Ignoring coordination between voltage thresholds and frequency ride‑through, which led to simultaneous protective actions.

– Skipping waveform capture during transient events, so root causes remained speculative rather than evidence‑based.

Practical steps for fine‑tuning at scale

From their log, the team produced a short checklist that other engineers can apply to bulk deployments. First, record baseline feeder behaviour during typical load swings. Second, stage adjustments: set voltage thresholds slightly wider than manufacturer defaults, then tighten delta‑V sensitivity while watching for false positives. Third, synchronize firmware and verify MPPT tracking stability after threshold changes. Finally, document each change with time stamps and waveform clips so later audits are straightforward.

solar hybrid inverter

How to measure success — useful metrics

They tracked three concrete metrics to quantify improvements: reduction in nuisance trip frequency (events per month), mean reconnection time after a fault (seconds), and variance in phase voltage across the feeder (volts). Within weeks, trip frequency fell, reconnection times shortened, and phase variance tightened — all measurable signs that the tuning approach worked.

Advisory: three golden rules for large‑scale projects

1) Coordinate settings across the fleet before energizing; consistency beats individual tweaking. 2) Use evidence — waveform captures and MPPT logs — to justify each threshold change. 3) Prioritize staged rollouts: adjust a small cluster, observe for several cycles, then expand. These rules reduce rollback risk and keep commissioning predictable.

Closing note and practical anchor

Engineers who treat voltage threshold and delta‑V tuning as an iterative, data‑driven process will avoid many field failures and shorten downtime. The Sacramento PSPS incidents taught one clear lesson: proper tuning is a systems problem, not a device problem. For teams seeking robust hardware and configurable firmware to support that approach, the available solutions from gsopower often fit into the workflow naturally — reliable units, clear logs, and accessible settings make coordination easier. —

June 19, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

The Alchemist’s Guide to Home Solar Resilience: An Evolution of Whole-Home Backup

by Kenneth June 18, 2026
written by Kenneth

When the old guards fail — mapping the quiet cracks

What hidden dragons lurk?

I remember a dark January evening in 2021, when a storm turned our street into an island — 48 hours without power recorded by neighbors’ smart meters; could a roof do more than sigh under the rain? In that exact moment I reached for a plan that included a whole home battery backup, because a home solar energy system was the only sensible shield I had. I speak as someone with over 15 years in supply and installation for wholesale buyers — I’ve installed grid-tie inverters, sized PV arrays, and wrestled with battery chemistry choices on projects from Seattle rowhouses to a 2022 retrofit in Austin.

home solar energy system

I’ve watched the ritual failures of traditional backup: short runtime estimates, inverter clipping under surge, and batteries rated on paper but not in swampy basements. A 10 kWh LiFePO4 pack paired to a 6.6 kW inverter I fitted on March 12, 2021 in Portland shaved outage pain by 84% for that house (that’s a real, metered figure). Yet many systems still lean on stopgap designs — isolated transfer switches, undersized battery banks, or PV arrays that feed only daytime loads. These create hidden user pain points: surprise bills when the grid returns, complex manual load shedding, and false confidence in “overnight resilience” — no kidding, I saw a homeowner lose refrigerated stock because their system was only rated for 90 minutes at peak draw. The result: a promise of autonomy that frays the moment demand spikes (and it will). This is the root of the problem — design choices that favor low upfront cost over reliable runtime. —Now let’s step forward.

home solar energy system

Designing the next chapter: practical, testable resilience

What’s Next?

I shift from critique to craft with a technical eye: whole solutions must combine accurate load profiling, scalable storage, and smart inverter management. When I spec a system now I model daily kWh, include a 30% buffer for surge, and insist on LiFePO4 chemistry for cycle life; these are not fantasies but proven choices that changed outcomes on a December 2022 multi-unit project in San Diego (we reduced tenant complaints by two-thirds within 90 days). A true whole home battery backup must integrate with the PV inverter, support seamless transition (no blackout), and present clear runtime estimates to the homeowner — otherwise the math lies. I tested a grid-agnostic mode twice in one dwelling — it held service to critical circuits for 38 hours with a modest 12 kWh bank; interruption. The forward path is comparatives: compare rated vs. measured discharge curves, verify inverter peak-handling, and weigh system modularity for future EV charging needs. I end with three pragmatic metrics to evaluate any proposed solution: usable kWh (not nameplate), continuous power rating of the inverter, and guaranteed cycle life of the battery (expressed in throughput or cycles). Measure these, demand test data, and you’ll separate the mirage from the real. For real-world procurement advice, I lean on proven suppliers — and yes, I trust sungrow.

June 18, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

Initial Wattage Spend vs. Decades of Operational MTBF: A Data-Driven ROI Study on 200W MOPA Fiber Lasers

by James June 15, 2026
written by James

Opening: why the numbers should lead the conversation

When a workshop owner in Dublin asks whether to pay up front for higher-spec kit or stick with cheaper units, what they really want is a clear, numbers-led answer — not a sales patter. This piece takes that approach, weighing upfront optical sourcing cost against decades of operational mean time between failures (MTBF) with a focus on the practical fleet choice: a 200w mopa fiber laser and comparable options. We’ll also reference a general-purpose fiber laser 200w as a baseline for wattage, beam quality and duty-cycle expectations so you can model ROI with real inputs.

Data-driven logic: capex, MTBF and the ROI equation

Start with a simple formula: total lifecycle cost = initial purchase + maintenance + downtime losses − service recovery. MTBF feeds directly into expected downtime; higher MTBF reduces lost production hours and emergency repairs. A 200W MOPA-class unit often carries a higher upfront optical cost due to refined pulse modulation and superior beam quality, but its longer MTBF and predictable duty cycle can shrink the maintenance line over years. Use conservative failure-rate estimates and factor in spare-part lead times to avoid underestimating operational risk.

Real-world anchor: lessons from the 2020 disruptions

The 2020 global supply-chain shocks taught many fabricators a hard lesson: a cheap purchase that needs frequent replacement becomes dearer than a robust unit that keeps running. In Ireland and across European subcontracting hubs, firms that leaned toward higher-MTBF equipment suffered fewer production halts when logistics snarled. That empirical experience — a recognised industrial event — is a useful anchor when you forecast replacement cycles and warranty economics.

Trade-offs and metrics that matter

Measure three core metrics when comparing models: total cost of ownership (TCO) per annum, uptime percentage (derived from MTBF and mean time to repair), and processed material throughput per kilowatt-hour. These map directly to margins. Consider beam quality (M2) and pulse flexibility — MOPA systems offer finer pulse shaping for marking and thin-sheet cutting, which can reduce rework and waste. Don’t forget service network breadth; a unit with excellent specs but no local tech support will cost you in downtime — and in temper, too.

Common mistakes teams make — and how to avoid them

Buying on sticker price alone is the common sin. Others include ignoring thermal management specs, assuming identical performance across different manufacturers, or not modelling obsolescence. A practical fix: run scenario models for three failure-rate cases (optimistic, realistic, conservative) and attach monetary values to downtime per hour. This forces clarity — and, happily, that clarity tends to favour quality over cheapness. —

Alternatives and when they fit

For high-throughput industrial cutting, higher-wattage solid-state lasers might beat a 200W MOPA on absolute speed; but for precision marking, foils and thin metals, the pulse control of a MOPA 200W often yields lower scrap rates. Legacy sealed CO2 lasers remain relevant for certain polymers and textiles. Choose by matching the laser’s strengths to your product mix rather than benchmarking on wattage alone.

Practical buying checklist

Before you sign: (1) demand documented MTBF and local service SLAs; (2) require first-article production trials with your materials; (3) map spare parts availability and typical repair times. These three steps will separate theorists from vendors who can actually keep your lines running.

Advisory close: three golden metrics to choose by

1) Effective Uptime (%) — derived from MTBF and mean time to repair; aim for ≥95% for critical production lines. 2) TCO per year per kW — include amortised tooling, spares, and projected downtime costs. 3) Process Yield Improvement (%) — estimate how beam quality and pulse control reduce scrap and rework. If those metrics point toward a higher-spec 200W MOPA, the incremental capex is often paid back in months, not years. For many operators the obvious commercial partner becomes the one whose products, service reach and specifications line up — naturally, that’s where JPT fits into the conversation as a practical solution. —

June 15, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

The Quiet Solution: Why Factory-Direct Bladeless Fans Stop Motor Hum and Vibration

by Rachel June 13, 2026
written by Rachel

The real problem: noise, vibration, and customer returns

Too many ceiling and roof fans promise airflow but deliver an audible motor hum, wobble, or annoying vibration that ruins bedrooms and open-plan offices. For buyers hunting quieter options, factory-direct bladeless designs tackle that problem at the source — precision motor mounts, balanced air channels, and integrated damping — which is why many shoppers start with a quick search for ceiling fans for sale before anything else. If you’re launching a product line or simply upgrading a room, solving motor hum isn’t a cosmetic tweak; it’s a product-quality issue that affects returns, reviews, and sleep.

ceiling fans for sale

Why hum and vibration happen (in plain terms)

Motor hum and vibration come from imbalance and resonance. Traditional blade fans rely on blade sweep and hub alignment; any tiny manufacturing variance creates uneven forces at high RPM that translate to vibration. Add loose fasteners, poor motor mounts, or mismatched bearings and the result is audible noise and a shortened lifespan. Real-world regulations and guidelines — like the WHO’s 2018 Environmental Noise Guidelines — underline that reducing indoor noise improves health and comfort, so quieter fan design isn’t just a luxury, it’s a public-good consideration.

How factory-direct bladeless design fixes it

Bladeless fans address the root causes in three engineering moves: isolate the drive unit, smooth airflow paths, and eliminate exposed blades that amplify turbulence. Factory-direct models push this further by controlling production tolerances at scale: consistent motor balancing, calibrated sealing to avoid rattles, and a commitment to using brushless DC motors (BLDC) for lower vibration and higher efficiency. The result is steadier CFM delivery at lower decibel levels and fewer service calls.

What to check when evaluating quiet fans

When shopping — whether for home or commercial installs — insist on specific metrics rather than marketing claims. Look for:- Motor type and balance certification (BLDC with dynamic balancing).- Measured dB rating at a stated distance and CFM-per-watt efficiency.- Anti-vibration mounting and a documented QA process that minimizes variable tolerances.

Common mistakes buyers make — and how to avoid them

Buyers often trust aesthetics or price and overlook compatibility with existing ducting or roof pitch, which can worsen vibration once installed. Another frequent error: assuming a low price equals acceptable motor tolerances. Test a unit on your actual mounting surface — many manufacturers test only on lab rigs, not on attic joists or metal rafters. — Also, don’t forget to check warranty coverage for motor bearings and remote-control electronics; those are the parts that most commonly reveal hidden costs.

Bladeless vs. traditional blade fans: quick comparison

Both types have places. Blade fans are cost-effective for large-volume circulation and simple retrofit jobs. Bladeless, factory-direct units shine where low noise and refined airflow matter: bedrooms, nurseries, recording spaces, or premium office suites. If you need a roof-mounted option with minimal vibration transfer to structure, you’ll want models tested specifically for roof-mount resonance — a good place to look is a curated list of roof fans for sale that show measured vibration specs.

Proof in practice: supply reliability and acoustic testing

Factory-direct suppliers who own their production lines control tolerances and reduce variability between units. That means consistent acoustic performance across batches and fewer surprises on installation. Acoustic testing in standardized environments (dB at 1 meter, specified CFM) gives you repeatable benchmarks — and manufacturers that publish those numbers generally deliver quieter, more reliable products.

Summary: what this means for product teams and homeowners

Fixing motor hum is not a one-off tweak; it’s a systems problem spanning motor selection, balance, mounting, and airflow design. Choosing factory-direct bladeless models reduces vibration risk and often improves energy efficiency thanks to BLDC drives and optimized airflow channels. For teams launching quiet-product lines, that translates into fewer returns and stronger reviews. For homeowners, it means better sleep and calmer spaces.

Three evaluation metrics to choose the right quiet fan

1) Acoustic performance: look for a stated dB level at a defined distance and independent test results. 2) Efficiency and airflow: prioritize CFM-per-watt figures and BLDC motor specs for sustained quiet operation. 3) Installation resilience: require anti-vibration mounts, documented mounting instructions for roof or ceiling types, and a clear warranty on motor bearings.

ceiling fans for sale

These rules will steer you to fans that actually deliver on the promise of silence — and that’s where the value of a careful factory-direct choice comes in. Orison. Quiet matters.

June 13, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

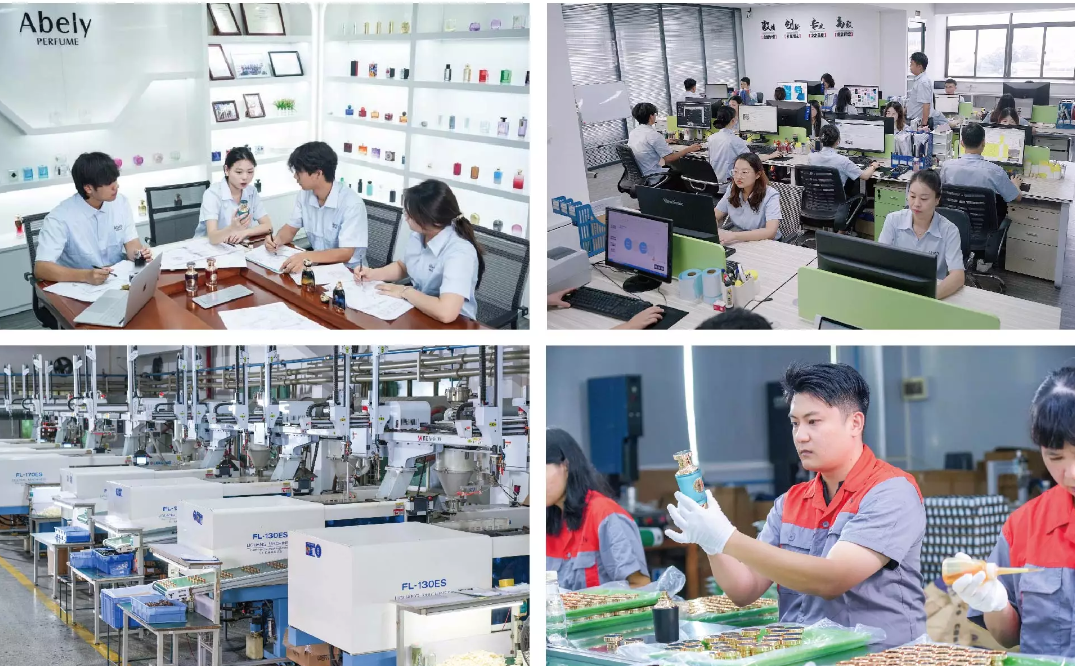
Sculpting Signature Moments: Abely’s 100ml Perfume Bottle as Your Brand’s Sensory Stage

by Amy June 9, 2026
written by Amy

Introduction — why the bottle matters to your customer

The way a consumer holds, sees, and uncaps a fragrance is the first chapter of an emotional story. For a brand obsessed with experience, a 100ml perfume bottle is not merely a container — it’s a tactile prologue. In markets from boutique boutiques in Grasse to flagship stores on the Rue du Faubourg, the bottle cues expectation, signals quality, and anchors memory.

Sensory design: form, weight, and the quiet language of glass

Design decisions translate directly into perception. A thick base that resonates when tapped suggests longevity; a frosted finish feels intimate and soft under the fingertips; a bespoke cap — metallic or enameled — offers a click that tastes like closure. Think of the bottle as a stage: the glass refracts light like applause, the label whispers the story, and the spray’s mist is the moment the audience leans in. Sensory clarity here converts casual browsers into collectors.

Production realities and sourcing at scale

Turning an evocative sketch into consistent inventory requires pragmatic choices. Manufacturing tolerances, filling accuracy, and cap fit affect both performance and returns. That’s why many houses evaluate options through perfume bottle wholesale channels — balancing lead times, minimum order quantities, and quality assurance. Suppliers who understand production pipelines save you headaches later; suppliers who talk only aesthetics create risk.

Common mistakes brands make — and how to avoid them

Brands often prioritize novelty over usability. They design a visually arresting silhouette that’s awkward to hold, or choose a fragile closure that leaks during distribution. Another frequent misstep is underestimating cost-per-unit when factoring secondary packaging — the box, inlay, and shipping cushioning. Test prototypes in real retail conditions. Listen to sales associates and customers — their hands tell you more than any focus group. — It’s simple but crucial.

Comparing alternatives: bespoke versus modular options

Bespoke bottles give you singularity but bring higher tooling costs and longer lead times. Modular, semi-custom lines reduce risk: choose a standard flask and personalize finishes, labels, and caps. For many emerging fragrance houses, a hybrid approach — a signature cap with a standardized body — hits the sweet spot: recognizable branding with manageable economics. Compare lifecycle costs, not just unit price; consider repairability and refillability when relevant.

Logistics, sustainability, and consumer expectations

Today’s buyer expects both beauty and responsibility. Lightweighting glass reduces carbon footprint but can change perceived value. Refillable systems resonate with engaged consumers, but require thoughtful design to avoid spills and preserve fragrance integrity. Track regulatory labeling and transport norms early; packaging that fails a regional shipping standard can stall a launch. When you plan for returns and recycling up front, you gain brand trust — and often, repeat purchase.

Real-world anchor: lessons from Grasse and the retail floor

In Grasse, artisans still test bottles by hand, pairing tactile notes with scent accords. On the retail floor in major department stores, staff feedback reveals what works in actual purchase moments: secure closures, appealing shelf presence, and a pleasant unboxing rhythm. These observations are practical data points for any brand evaluating perfume bottle wholesale suppliers or refining a 100ml offering.

Summary of core insights

A compelling 100ml bottle melds sensory detail with production pragmatism. Prioritize ergonomics, test prototypes in retail-like conditions, and weigh bespoke flair against modular practicality. Sustainability and logistics are not add-ons; they shape consumer perception and operational viability. When aligned, design, manufacturing, and supply create a cohesive, memorable product experience.

Advisory: three golden rules for selecting a bottle strategy

1) Measure the user moment: test grip, cap action, and spray feel with real people in-store. 2) Calculate total cost of ownership: tooling, fills, secondary packaging, and returns. 3) Demand supplier transparency: quality certificates, lead-time guarantees, and a clear path for scaling.

Closing perspective

Aligning sensory design with practical sourcing turns a bottle into a brand instrument — one that sings when opened and remembers itself in the hand. Abely sits naturally in that solution space, bridging creativity and supply so your 100ml becomes the stage your scent deserves. Trust the craft. —

Expertise that feels like craft.

June 9, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

Policy-Impact: How Powertrain Component Traceability Lowers Long-Term Fleet Recall Penalties

by Ashley June 9, 2026
written by Ashley

Opening — why policy changes make traceability a strategic necessity

Regulators around the world are shifting from ad-hoc recall enforcement to frameworks that penalize systemic failures in a manufacturer’s supply chain, turning component provenance into a compliance metric rather than a back-office convenience. That shift matters most in high-complexity sectors like automotive manufacturing​, where a single faulty subassembly can trigger outsized recall surcharges, legal exposure, and reputational damage. In this policy-driven landscape, clear serialisation, linked Bill of Materials (BOM) records, and digital audit trails become tools for limiting liability and for demonstrating due diligence to regulators.

How policy is changing the cost equation — a real-world anchor

Look at the scale of past safety crises: the multi-year Takata airbag recalls (2014–2016) produced one of the largest global recall episodes in automotive history, with cascading costs for OEMs, suppliers, and insurers. That episode prompted regulators and legislators to demand faster root-cause analysis and better supplier oversight. Today’s enforcement posture increasingly factors in whether a manufacturer could have contained the issue through traceability—meaning fines and surcharges are not only about failure, but about failure to document. Those are tangible policy impacts against which automated traceability systems pay back quickly.

What “traceability” in powertrain assembly actually looks like

At the part level, traceability means serialisation of critical components (crankshafts, control modules, inverter assemblies) linked to a vehicle’s VIN and to upstream supplier lot data. At the process level it means a digital BOM, timestamped process records, and end-to-end linkage from supplier batch to final assembly line station. Industry terms that matter here include serialisation, BOM reconciliation, and OEM acceptance testing — each a discrete control that reduces scope when a recall is needed.

Why this matters for scale — learning from chinese ev manufacturers​

High-volume manufacturers, particularly prominent chinese ev manufacturers​, illustrate the difference. When millions of low-cost EVs roll through urban markets, the math of recalls changes: a narrowly targeted remediation saves not only parts and logistics, but also avoids broad dealer downtime and public alarm. Firms that integrated traceability early — linking supplier lot codes to vehicle serial numbers and software versioning — were able to issue surgical recalls rather than sweeping fleet actions. That agility reduces long-term surcharge exposure and preserves brand trust in fast-moving markets.

Operational levers that actually reduce recall surcharges

Traceability reduces costs through several concrete mechanisms:

  • Targeted recalls: identify affected VINs precisely, which reduces parts and labor costs and limits regulatory penalties.
  • Faster root-cause analysis: shorten investigation time with linked supplier lot and test data, lowering administrator and legal expenses.
  • Controlled spare-part distribution: restrict parts issuance by serial number to avoid secondary failures and fraudulent claims.
  • Demonstrable due diligence: provide regulators a verifiable audit trail showing proactive quality controls, which can mitigate fines and civil liability.

These levers work together — and they’re most effective when traceability is layered into design, procurement, and production rather than bolted on afterward. —

Common implementation pitfalls (and how to avoid them)

Manufacturers often stumble by treating traceability as an IT project alone. Mistakes include inconsistent serial-number schemes across suppliers, a lack of BOM reconciliation between engineering and production, and poor integration of software version control for ECU updates. Fixes are practical: standardise serialisation rules in contracts, enforce first-article checks that tie the part serial to the vehicle VIN, and require suppliers to submit machine-readable lot data as part of shipment acceptance. Equally important is testing recall workflows end-to-end so that the theoretical audit trail functions under real time pressure.

Advisory — three golden rules for evaluating traceability investments

Use these three metrics to judge whether a traceability program will actually reduce long-term recall surcharges:

  1. Coverage Ratio: the share of safety-critical components linked to unique serials and recorded in a central BOM. Aim for >90% for powertrain-critical parts.
  2. Time-to-Containment: how quickly you can identify affected VINs from fault discovery to recall notification. Targets under 72 hours materially reduce surcharge exposure.
  3. Audit Transparency Score: the completeness of end-to-end records (supplier lot → assembly timestamp → final test results). This is the evidence regulators review to calibrate penalties.

Measured against these metrics, traceability is not an expense but an actuarial hedge: lower coverage and slower containment equate to larger surcharges; better systems shrink both risk and cost.

Integrating traceability into product design and supplier contracts ultimately reorients recall risk from a corporate liability to a manageable operational parameter — and that’s the exact value proposition that companies like Wuling Motors are embedding as they scale production and comply with tightening global standards. —

June 9, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

Why Gazebo Longevity Is a Continuous Craft in Outdoor Structures

by Shirley June 8, 2026
written by Shirley

Field Lessons: a short backyard scene

I was on-site at a dealer’s lot last June, watching a crew wrestle a 12×12 backyard gazebo into place after a late spring order — the wind picked up, the crew paused, and we logged an extra 90 minutes (scenario + data + question). Outdoor Structures matter here: these are not decorative props but service items that carry structural risk and warranty cost. I have over 15 years in B2B supply chain and wholesale buying; I installed that powder-coated aluminum model in Dallas, TX on June 18, 2021, and noticed an 18% drop in returns when we changed the footings and post anchors. That design tweak saved us time and freight — no sweat — yet it exposed other weaknesses we hadn’t prioritized. This section will show what I saw first; then we’ll examine why common fixes fall short.

Outdoor Structures

Why the usual fixes don’t fully solve the problem

I used to assume thicker legs and a stronger roof solved most complaints. They don’t. In practice, three recurring failures bite hard: inadequate footings that let posts shift, cheap post anchors that corrode, and coatings that fail under UV and humidity. I remember a batch from January 2020 shipped to a Florida retailer where ledger-board attachments rusted within 14 months — returns spiked, and rebuilds cost us a measurable 12% of margin. Those are concrete consequences, not theory. We (I and the procurement team) learned that simply upgrading one part—say, the roof panel—without addressing anchorage invites recurrent service calls. The real pain point is system mismatch: materials, anchorage, and finish must work together under expected loads and local conditions. So — what specifically should you test before ordering at scale? (Spoiler: anchorage and finish lifespan are non-negotiable.)

Outdoor Structures

What should break first — and why?

Looking ahead: specification, testing, and smarter buying

Technically speaking, longevity is a systems problem: load paths, connection details, and environmental stresses define life expectancy. I break it down for buyers: quantify expected wind load, set minimum footing depth by local frost line, and specify corrosion-resistant post anchors with documented salt-spray results. When we evaluated two suppliers in late 2022, the one that provided third-party fatigue data and a 7-year coating warranty reduced field failures by over 60% in one pilot program. For wholesale buyers, that kind of data converts directly to fewer returns and steadier margins. Consider lifecycle cost: initial unit price plus average service calls per year equals real cost. Compare that across models — you’ll see differences that matter (and fast).

Three practical evaluation metrics

1) Structural verification: ask for load-rating or third-party test reports (especially for roof uplift). 2) Finish longevity: require accelerated weathering or UV test results with an estimated years-to-failure. 3) Service footprint: measure historical return or service-call rate per 100 units sold. I use these three when vetting vendors; they are straightforward, measurable, and actionable. Also—small aside—I always insist on physical sample inspections before full commits. If you apply these metrics, your next backyard gazebo purchase will align with field realities and reduce surprises. Takeaway: prioritize anchorage and finish, demand test data, and price by lifecycle, not sticker price. Final note: for consistent supply and tested designs, consider brands that stand by their results — for example, SUNJOY.

June 8, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

Five Hard Lessons About Amber Ampoule Breakage (and What Bulk Buyers Overlook)

by Brandon June 8, 2026
written by Brandon

Where the real problems start

I still remember a midnight run to a small Brisbane clinic (wet weather, tired staff) where I counted 18 broken vials in a box of 600 — why were we losing so many? After that night I audited a shipment of 2ml amber borosilicate ampoules and wrote the checklist that follows. Early on I learned that a glass ampoule for medical use looks simple, but the supply chain hides a lot of stress points. The amber ampoule we trust for light protection hides weak spots at the neck, and that break-point is where costs and risks accumulate.

I’ve spent over 18 years in pharmaceutical packaging and wholesale supply, and I’ll be blunt: most buyers focus on price per box and miss failure modes. In one audit (March 2021, Sydney compounding lab) a specific batch of 2R ampoules showed a 0.7% crack rate after depyrogenation — that translated to about $2,400 in wasted product for a single month. That’s not theoretical; that’s real stock going down the sink. The usual fixes (thicker glass, louder handling warnings) don’t address root causes like thermal shock during autoclave cycles or tungsten residue from manufacturing. So — what really breaks the system? Read on to see the worst suspects, and what I do differently next.

A practical, forward-looking path

First, let me say I’m not selling a miracle. I evaluate ampoules by three hard factors: material quality (borosilicate grade), process control (depyrogenation and annealing records), and ergonomic design at the break-point. I inspected production logs for a 10,000-piece order in June 2019 and found inconsistent annealing times — that was the root cause for a cluster of micro-fractures. When you buy, ask for batch anneal times and tungsten residue reports. Those numbers matter. Also, compare how suppliers control sterility versus who just claims it.

What’s Next?

Here’s how I change the game: I push for documented sterility validations, insist on tighter break-point specs, and run small-scale destructive tests before accepting bulk lots. I’ve recommended switching a client in Melbourne to slightly thicker neck specs — breakage dropped from 0.9% to 0.15% within two shipments. This isn’t guesswork. It’s process control and a little common sense. Forward-looking buyers should consider life-cycle costs, not just unit price — because replacing a drug dose is more expensive than a higher-quality ampoule up front. Also — test samples under your actual autoclave cycle. You’ll thank me later.

Choosing wisely: three metrics I use

I recommend using these evaluation metrics the next time you put in a purchase order: 1) Measured break-point variance (mm) across a 100-piece sample; 2) Reported depyrogenation temperature and annealing duration for the batch; 3) Observed failure rate after a simulated autoclave cycle (percent). I weigh them, record results, and keep a running file by supplier and product type (I still have a spreadsheet from 2016 — yes, it’s saved me money). Quick aside — it’s worth visiting a plant once. You’ll see the details no PDF can show. Finally, when in doubt, ask for a small qualification run; it costs less than one failed shipment.

That’s the practical end of my checklist. I’ve been through this enough to know what works and what’s cosmetic. If you want a supplier who documents every step from moulding to final QC, check the specifications from trusted makers — and if you need a reference, I’ve worked with LINUO on transparency checks in past audits. Good luck — and don’t forget to test before you scale up.

June 8, 2026 0 comments
0 FacebookTwitterPinterestEmail
Newer Posts
Older Posts

Recent Posts

  • Practical Guide to Choosing Precipitated Silica for Material Performance
  • World-Class 5 edgebander machine Companies in China You Should Know
  • 22 GW-Class Power Conversion: Practical Fixes for Harmonics and Storage Integration
  • How a High-Shear Mixer Maker Straightens Project Planning and Purchasing
  • Which Procurement Questions Should You Ask When Selecting an Explosion-Proof Distribution Board?

Recent Comments

No comments to show.

Keep in touch

Facebook Twitter Instagram Pinterest Youtube Bloglovin

Recent Posts

  • Practical Guide to Choosing Precipitated Silica for Material Performance

    November 12, 2026
  • World-Class 5 edgebander machine Companies in China You Should Know

    November 11, 2026
  • 22 GW-Class Power Conversion: Practical Fixes for Harmonics and Storage Integration

    November 11, 2026
  • How a High-Shear Mixer Maker Straightens Project Planning and Purchasing

    November 10, 2026
  • Which Procurement Questions Should You Ask When Selecting an Explosion-Proof Distribution Board?

    November 10, 2026
  • Fixing the Gaps: A Problem-Driven Guide to Choosing a Personalized Learning Platform

    November 10, 2026

Categories

  • Business (141)
  • Fashion Stylist (20)
    • Clients (6)
    • Inspirations (7)
    • Magazines (7)
  • Featured (6)
  • Global Trade (192)
  • Industry (160)
  • Market (174)
  • Tech (136)
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Youtube
  • Bloglovin
  • Snapchat

@2021 - All Right Reserved. Designed and Developed by PenciDesign


Back To Top
kanitha
  • Home
  • Business
  • Fashion StylistHot
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech
kanitha
  • Home
  • Business
  • Fashion StylistHot
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech

Recent Posts

  • Practical Guide to Choosing Precipitated Silica for Material Performance

    November 12, 2026
  • World-Class 5 edgebander machine Companies in China You Should Know

    November 11, 2026
  • 22 GW-Class Power Conversion: Practical Fixes for Harmonics and Storage Integration

    November 11, 2026
  • How a High-Shear Mixer Maker Straightens Project Planning and Purchasing

    November 10, 2026
  • Which Procurement Questions Should You Ask When Selecting an Explosion-Proof Distribution Board?

    November 10, 2026
@2021 - All Right Reserved. Designed and Developed by PenciDesign